Aluminum Casting Leak at the Bend: Why Visual Checks Fail
The inner bend of a flanged elbow can leak after every surface check passes. Shrinkage there is a feeding problem, so the fix sits in the gate (the inlet) and the riser (the feeder reservoir). A 0.9 MPa test held for 60 s is the acceptance criterion.
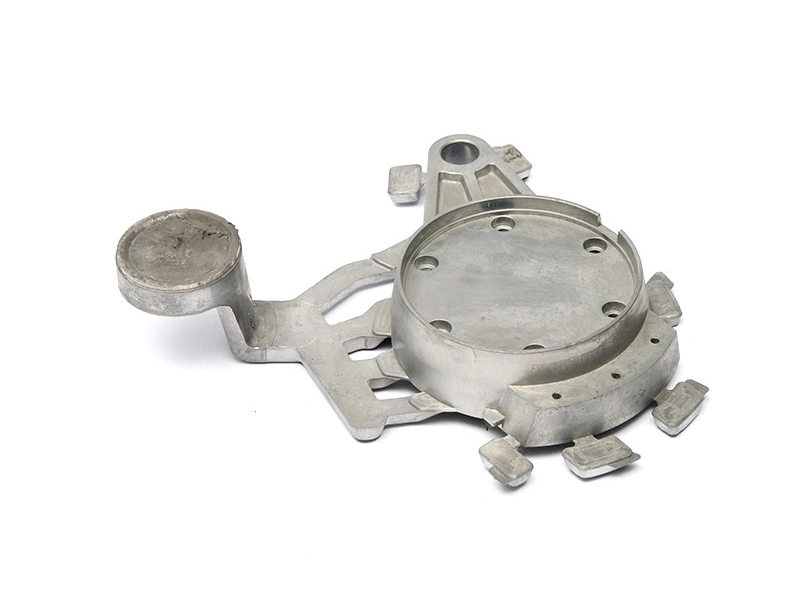
A 75×60×55 mm elbow in A356 (GB/T 1173 ZL101A, pending confirmation) weighs 150±20 g and is cast by metal-mold gravity casting in the as-cast F temper, with no T6 heat treatment. The Ø60±0.5 mm flange and the 0.05 mm flatness are drawing targets; the gate and riser positions are set at the tooling review, pending foundry confirmation.
Why does an aluminum casting leak at the elbow bend?
The 150 g elbow puts its thickest section at the inner bend. That mass freezes last, and a hot spot is a zone that solidifies after its neighbors, so it needs feed while the thinner walls have already set. When that feed runs short, the last metal pulls apart into connected porosity, a pore network through the wall.
A cutter cannot create that path. Turning the flange face to 0.05 mm flatness, or boring the Ø20 H9 port, removes metal only where the drawing calls for it; neither opens a way through a 4–6 mm wall. A leak that appears after machining was cast in, so a second lathe pass will not close it and the mold has to change.
Where does shrinkage form in a 4 to 6 mm elbow wall?
Shrinkage forms where sections meet. In this 4–6 mm wall, the inner bend joins the flange disc and the tube, so the metal there carries more mass than the tube wall or the flange disc alone, and that is where the leak path starts.
Why can a visual check miss a leak in the bend?
A visual check reads the skin, and the skin over a 4–6 mm wall is the densest part of the casting. Shrinkage sits below it, so a magnifier adds resolution, not depth, and the surface reads closed. Penetrant testing, or PT, is run on machined surfaces and finds defects that break them; it does not look inside the wall.
That gap lets an elbow pass a visual check and still leak at 0.9 MPa. The pressure test is the bend criterion, and PT is a surface check with a different job. Using one for the other releases a leaking part after the machining cost is spent.
How does a 0.9 MPa pressure test find a bend leak?
The test clamps the flange and the port, fills the part, and holds 0.9 MPa for 60 s. A connected pore path lets the medium through, and the leak shows at the bend. It runs after turning the flange face and the port and after drilling the flange holes, so the leaking part has already paid for its machining.
The 0.9 MPa test is the acceptance criterion for release. It is not a pressure rating for this casting, and neither is the 0.6 MPa figure, a typical working pressure for the line this part serves, to be confirmed on the drawing.
| Check | Target (mm or MPa) | Allowed range | Measured with |
|---|---|---|---|
| Bend leak | 0.9 MPa, held 60 s | No leak through the wall | Pressure test bench |
| Flange face | 0.05 mm flatness (to be set by the drawing) | 0.05 mm blade must not enter, free part | Plate and feeler gauge |
What mold changes keep the bend from shrinking?
Two positions set the feeding path: a gate on the outer bend and a riser at the flange end. If the current mold has its gate at the inner bend and its riser at the port end, the hot spot is the entry point. The outer bend fills last, and the inner bend freezes last, cut off from the riser by the thin tube. With the gate at the outer bend, the bend fills from outside and the riser feeds the inner wall. At the flange end, the riser holds liquid against the heavy flange, so the inner bend draws as it freezes.
Wall thickness at the bend comes from the drawing before the mold is cut. A thicker bend changes the feeding distance, the 150±20 g mass and the mold, so the section belongs in the RFQ package. Ask how large the riser must be for a 4–6 mm wall, and how many consecutive first articles pass 0.9 MPa over 60 s before tooling acceptance.
The decision is a tooling one: gate side, riser end and bend section on one drawing. Send it with the 0.9 MPa test callout, and the quotation separates mold work from turning and testing.