Passivation vs Phosphating on 45 Steel Brackets?
Passivation vs phosphating 45 steel is a drawing question before it is a process question. On a medium-carbon bracket, passivation leaves no chromium-rich film to re-form, so the finish that usually fits is phosphating or black oxide. The surface finishing route follows the callout on the drawing, not a shop default.
Carbon Steel Does Not Passivate Like Stainless
Passivation on stainless steel is an acid clean, and the passive film re-forms afterwards because the alloy holds enough chromium to rebuild its oxide. 45 steel to GB/T 699-2015, quenched 840–860 °C and tempered 550–600 °C (both typical windows) to a hardness of 220–250 HB, holds no such reservoir. An acid bath strips free iron and scale, and what comes out is clean carbon steel that will flash-rust in a humid room.
The word still turns up on carbon steel drawings. It usually means one of two things: a passivation step after zinc plating, acting on the plating rather than on the steel, or a loose way of writing a conversion coating that the author meant as phosphating. Neither reading is safe to assume from the word alone.
Three Callouts, Three Processes
Passivation, phosphating, and black oxide leave different things on the surface, so they cannot share one acceptance line. The table separates them where a drawing has to choose.
Callout on the drawing | What it leaves on 45 steel | Where it is the right call | Goods-in check |
|---|---|---|---|
Passivation | No film on bare steel; a thin film only on a plated layer | Stainless parts, or carbon steel after zinc plating | Free iron and water-break |
Phosphating | A gray phosphate crystal layer that holds oil | Bare 45 steel that will be oiled or painted | Coverage and the coating class on the drawing |
Black oxide | A thin dark oxide, kept oiled | Indoor handling where a dark finish is wanted | Color, oil film, and a rub check |
All three follow the same preparation on this bracket: blast to Sa 2.5 to ISO 8501-1 before the mounting face is machined, then finish after machining. The blast cleans the surface. It does not pick the finish.
Why the Drawing Decides, Not the Shop
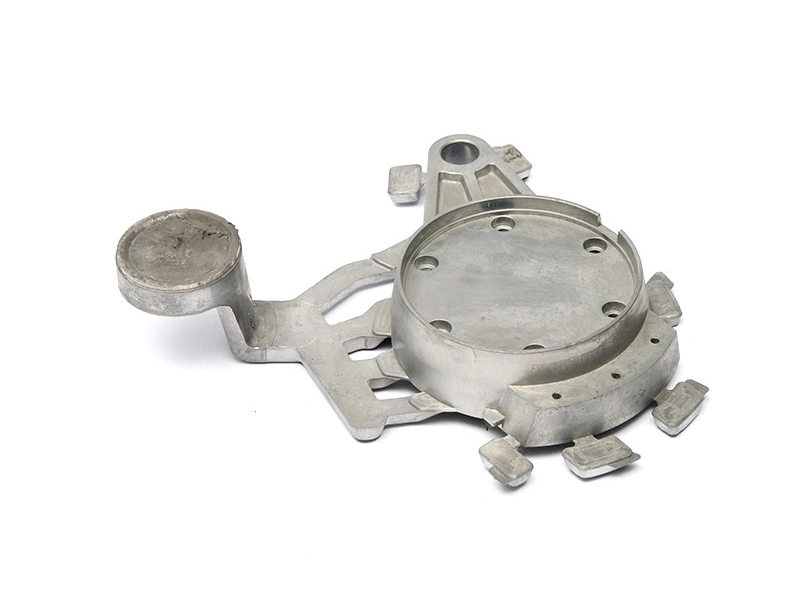
The metal casting route for this bracket ends with the finish held for drawing confirmation, because the shop has no basis to choose one. The same sheet already carries the design targets: ≥355 MPa yield and a ±0.2 mm hole pitch. The finish line belongs there too, with a standard number beside it.
A shop that falls back on its usual finish ships parts that look right and fail at goods-in. The inspector compares the surface to the callout. Write "surface treatment" and the answer is a question; write one process word and a standard, and the answer is a route.
The purchase order should repeat the drawing word for the finish, not paraphrase it. A paraphrase is where phosphating becomes passivation in transit.
What Goes Wrong When the Callout Is Wrong
Two failures cover most cases. A drawing that says passivate and a shop that phosphates produces a gray crystalline surface where the inspector expected bare metal, and the batch is rejected on appearance before any test runs. A drawing that says phosphating and a shop that acid-cleans ships bare steel with no barrier, which rusts in transit or in the warehouse.
Either way the part is stripped and refinished, or accepted by concession with the finish logged as a deviation. The cost lands on the batch. A non-cosmetic, oiled part in a dry warehouse may never show the difference, but the drawing should still be corrected before the next order.
How to Close It Before the PO
Put one process word on the drawing, not a category. Add the standard the finish will be judged against, say whether a plated layer sits under the callout, and ask for a coupon or a first article with that finish before the batch is released. The finish follows the machined mounting face here, so the coupon should come from a part that has seen the same blast and cut.
If the drawing is silent, the RFQ answer is a question about the finish. That question costs one email. The wrong default costs a batch, a strip, and a second inspection.
Send the drawing with the finish line written, and ask for that line to be repeated in the quote, standard included.