What Should Buyers Compare When Choosing Casting Part Suppliers?
Buyers should compare casting part suppliers by the supplier's fit for the specific part, not by a general equipment list, company size, or lowest first quotation. The comparison should cover the proposed casting process, alloy control, tooling ownership, feature and datum plan, machining and finishing scope, inspection evidence, traceability, capacity assumptions, and response to changes or nonconformances. Each supplier should answer the same drawing-specific questions so that purchasing does not compare a finished component from one bidder with a cast blank from another.
Begin with the part's function. Mark pressure boundaries, sealing faces, bearing or locating surfaces, threaded holes, cosmetic zones, and features that can remain as cast. Then identify likely risks such as shrinkage near a heavy boss, distortion in a long wall, core movement, flash at a shutoff, or a pore opened by machining. A supplier is a better fit when it can connect each risk to a process control and a verification method.
Compare Process Fit
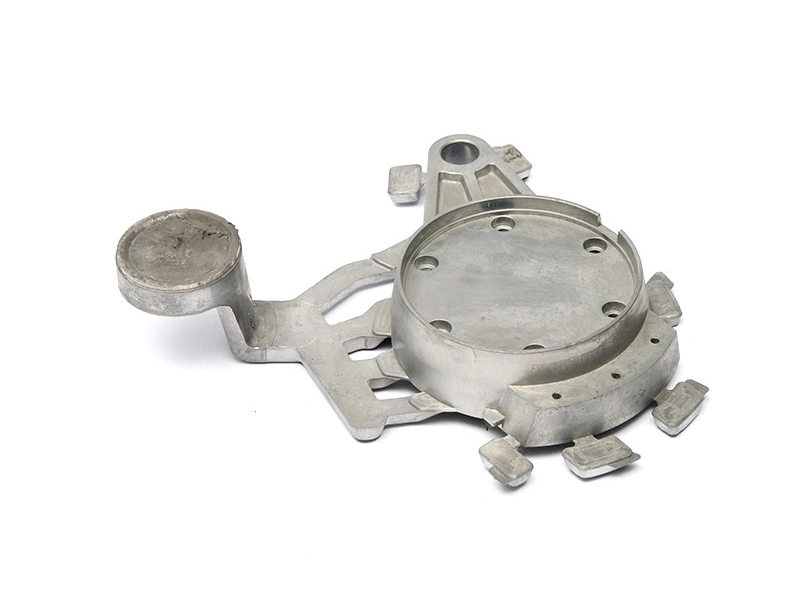
Different casting routes suit different geometry, volume, alloy, surface, and tooling requirements. Sand casting, gravity casting, die casting, investment casting, centrifugal casting, and machining from stock should not be treated as interchangeable services. Ask the supplier to explain why the proposed route fits the wall, cores, draft, section transitions, quantity, and finished state. If a feature requires machining or a design change, that should be visible in the technical response.
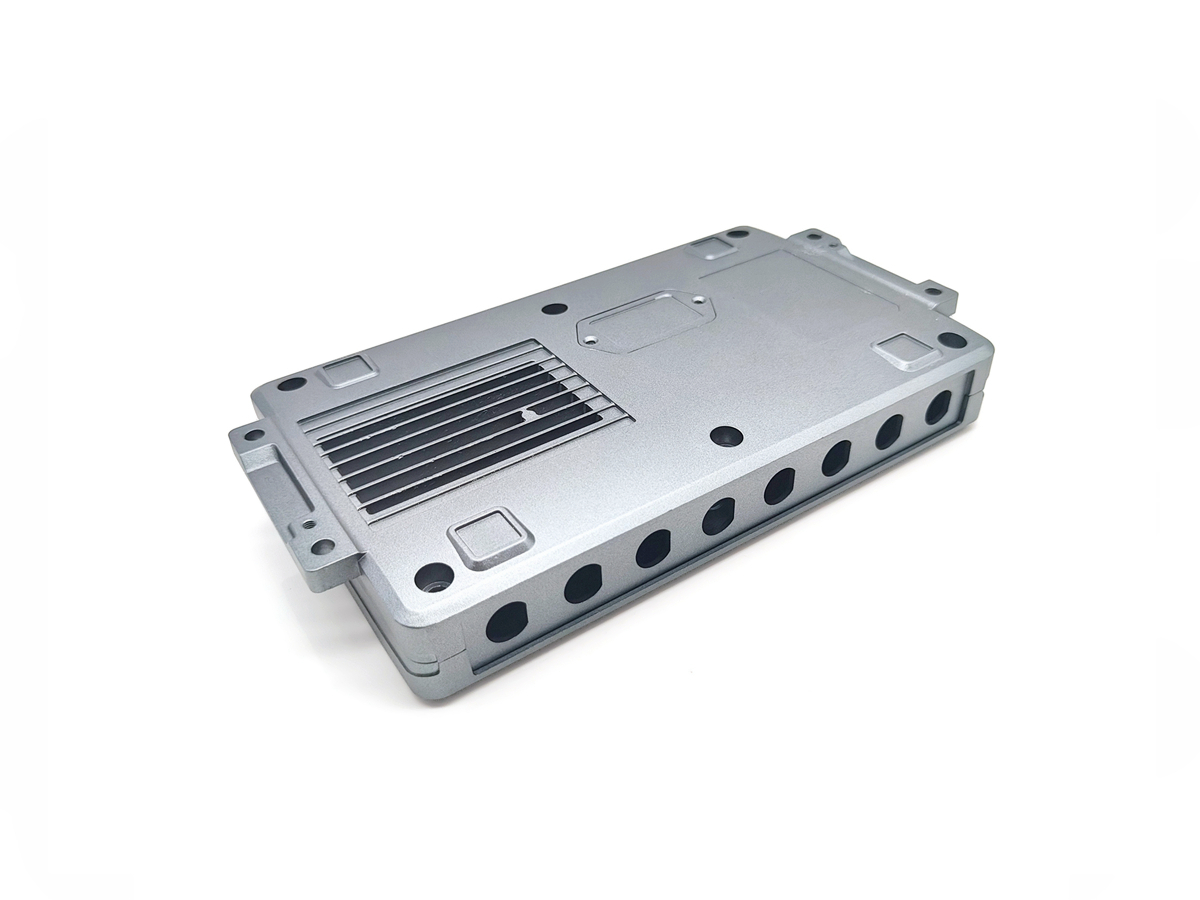
The metal casting service scope should be reviewed with the actual drawing and the required delivery state. A supplier that can cast the shape may still be unsuitable if it cannot establish the final bore, pressure surface, datum, finish, or inspection report needed by the buyer.
Compare Material and Tool Control
Ask how the alloy is identified, received, stored, melted or charged, and linked to the production lot. The buyer should define the exact designation, approved alternatives, condition, and records required. Do not accept a broad statement such as “aluminum alloy” or “bronze available” when the drawing depends on a particular material or customer restriction.
Tool control is equally important. Confirm who designs, owns, stores, maintains, repairs, and approves changes to the die, pattern, core box, trim tool, fixture, or gauge. Ask how a tool repair is recorded and how the affected part lot is identified. The tool decision is part of supplier selection because a low part price may be less valuable if the buyer cannot access the tool data or control future modifications.
Compare Finished-Part Evidence
Request a sample quality package before award. It may include material records, dimensional results, visual limits, internal examination, leak or pressure testing, surface inspection, machining records, and approved deviations. The required evidence should match the function. A visual inspection may suit a cosmetic surface, but it does not establish a pressure boundary. A material certificate supports identity, but it does not prove a threaded assembly will seal.
When the part is machined, include the post-machining scope in the comparison. Ask whether the supplier controls datums, fixturing, allowance, burrs, cleaning, and final measurements. The quote and the evidence package should describe the same finished state.
Compare Commercial Risk Without Guessing
Comparison area | Ask the supplier to show | Buyer decision |
|---|---|---|
Process route | Why the route fits the geometry and quantity | Whether the proposed process is technically suitable |
Material control | Alloy identity, lot link, and approved alternatives | Whether the material risk is controlled |
Finished scope | Cast, trim, machine, finish, clean, and test operations | Whether quotes describe the same deliverable |
Evidence and change | Inspection, traceability, deviations, and change response | Whether future problems can be isolated and resolved |
Separate tooling, casting, trim, machining, finish, inspection, testing, packaging, freight, samples, and rework. Ask each supplier to list assumptions about quantity, batch size, material, scrap or sorting, customer-supplied tooling, and subcontracted operations. A schedule should also identify dependencies such as drawing release, tool approval, trial corrections, finish approval, and first-article inspection. Avoid converting a general capacity statement into a fixed delivery promise without those inputs.
Finally, compare how the supplier handles change. Ask for the notice process, approval authority, old-stock control, deviation format, and record retention. The best supplier is the one whose technical, quality, and commercial response can be checked against the same released part. That is a more defensible decision than choosing from a directory or ranking suppliers by a single headline capability.
For a final short list, ask each supplier to identify one feature that drives cost and one feature that drives quality risk. The answers reveal whether the supplier has actually studied the part. Record the response with the quote revision, because a later change to the die, machining route, subcontractor, or inspection plan should be compared with the assumptions used for the award.
The metal casting service scope should be evaluated together with the buyer's drawing and acceptance plan. A supplier comparison is complete when the buyer can explain not only who can make the casting, but also how the selected supplier will prove the delivered part is the right one.