How Are OEM Die Casting Part Changes Controlled?
OEM die casting part changes are controlled by identifying the affected requirement, assigning a new or approved revision, reviewing the effect on tooling and process, and validating the delivered state before production release. A change can involve the drawing, 3D model, alloy, heat condition, die, insert, gate, cooling, trim, machining, surface treatment, packaging, inspection, or supplier. The size of the change does not determine its importance; the affected function and evidence do.
The starting point is a clear baseline. Record the approved drawing and model revision, material, tool identity, process route, machining and finish condition, inspection plan, and open deviations. Without a baseline, the team may compare a new sample with an earlier part that was already made under different assumptions. The buyer should know what the supplier is changing and what remains unchanged.
Classify the Change by Risk
A drawing change to a mounting face, sealing land, pressure wall, thread, bore, or datum usually requires direct engineering review. A material or heat-condition change can affect casting, machining, strength, corrosion, or finish. A die repair can change flash, draft, wall, cooling, or local geometry. A machining fixture or program change can affect position and repeatability. A packaging change can affect cleanliness or damage even when the metal geometry is unchanged.
Classify the change by the failure it could introduce. Ask whether it can affect fit, seal, load, pressure, appearance, corrosion, conductivity, wear, assembly, or traceability. Then define the smallest evidence that can answer the risk. This avoids both extremes: releasing an important change with only a verbal note, or repeating every qualification test for a clerical revision that has no product effect.
Change | Potential effect | Review evidence |
|---|---|---|
Drawing or model feature | Fit, seal, load path, wall, or assembly | DFM review, sample dimensions, and functional check |
Alloy or material source | Castability, properties, machining, or corrosion | Material records and application-specific comparison |
Die repair or insert | Flash, draft, cooling, local geometry, or cycle | Tool inspection, sample comparison, and affected feature check |
Machining or finish | Datum, tolerance, surface, fit, or contamination | Route revision, final inspection, and assembly or finish test |
Approval and Validation
Set the approval authority before the change is implemented. The buyer's engineering, quality, purchasing, and supplier teams may each have a role. The change record should identify the reason, affected documents, affected tools, risk review, samples, tests, disposition of old stock, and release date. If a customer or regulatory approval is required, it should be part of the gate rather than an afterthought.
Approve the sample in the state the OEM will receive. A raw casting sample may show a die change but cannot prove a final machined thread or coated surface. A dimensional report may show a feature but not a leak, assembly, wear, or pressure result. The evidence should follow the risk identified in the change review.
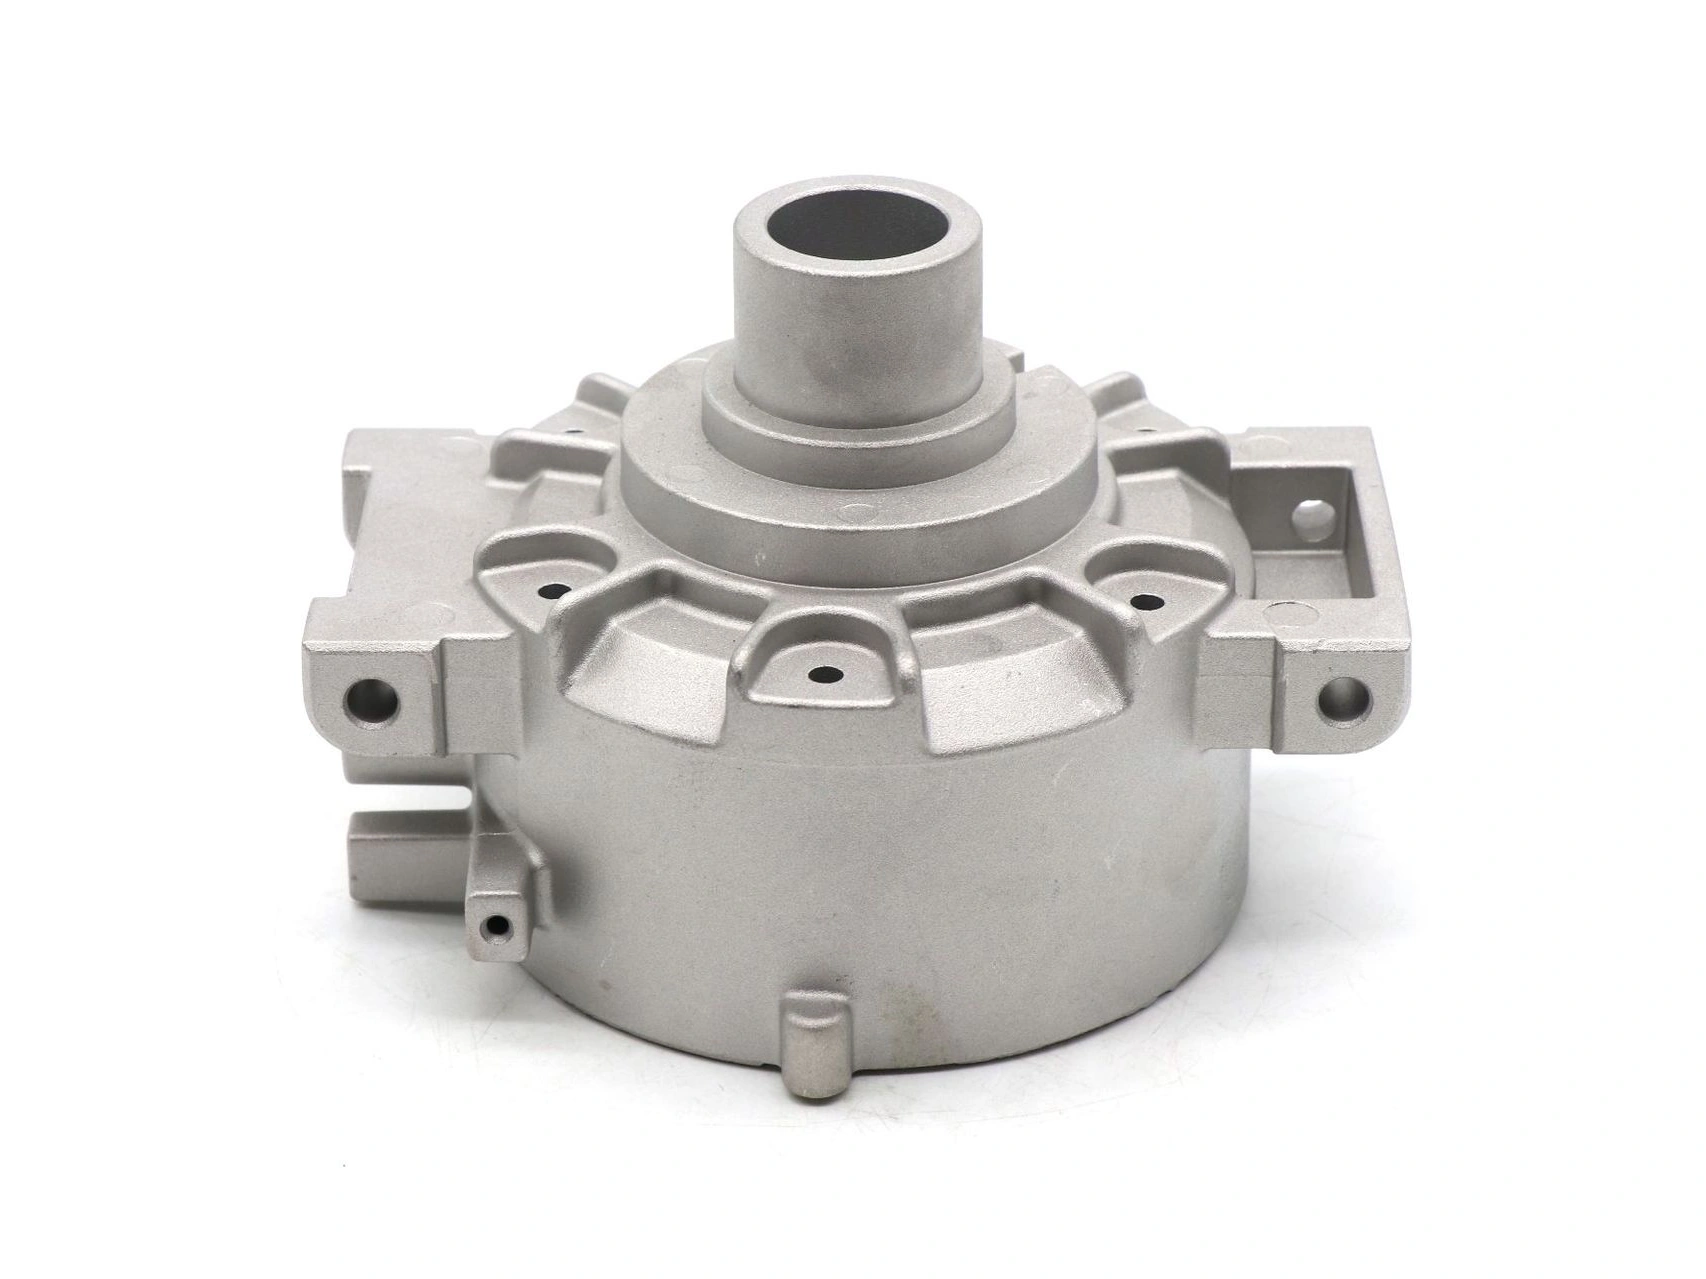
Neway's aluminum die casting service can be evaluated with the released material, tool, and process baseline. When a machining change affects interfaces, include the post-machining route in the validation rather than approving the casting and machining separately without checking the completed part.
Control Traceability and Old Stock
Identify the first lot produced under the new revision and the last lot under the old one. Decide whether old stock can be used, reworked, or must be segregated. Mark containers, inspection reports, and deviations so mixed revisions do not enter the same assembly. If the change is a supplier process change with no drawing revision, the production record should still identify the effective date, tool or route, and approval.
After launch, review field feedback, inspection trends, repairs, and nonconformances against the change history. If the part behaves differently, the team can trace the difference to a specific tool, material, machining, finish, or supplier state. This is the practical benefit of change control: it makes a production decision explainable.
Questions for the Buyer and Supplier
Ask what changed, why it changed, which part features are affected, what documents and tools changed, whether old stock is mixed, which sample represents production, and what evidence closes the risk. Put the answers into the change record and the purchase quality agreement. Do not treat a supplier's statement that “form, fit, and function are unchanged” as sufficient without identifying how the conclusion was checked.
OEM die casting changes are controlled when a known baseline, risk-based evidence, revision identity, and traceability meet at the release gate. That keeps the part stable for the OEM while allowing the supplier to improve tooling and process under documented approval.
Use an effective-date rule that the production and receiving teams can apply. The change notice should identify the first acceptable lot, the last lot made to the previous state, and the disposition of work in process. If a change is urgent, record the temporary approval, expiration condition, and follow-up validation instead of allowing an emergency instruction to become an undocumented permanent process. This gives purchasing and quality the same answer when material from different revisions is in transit.