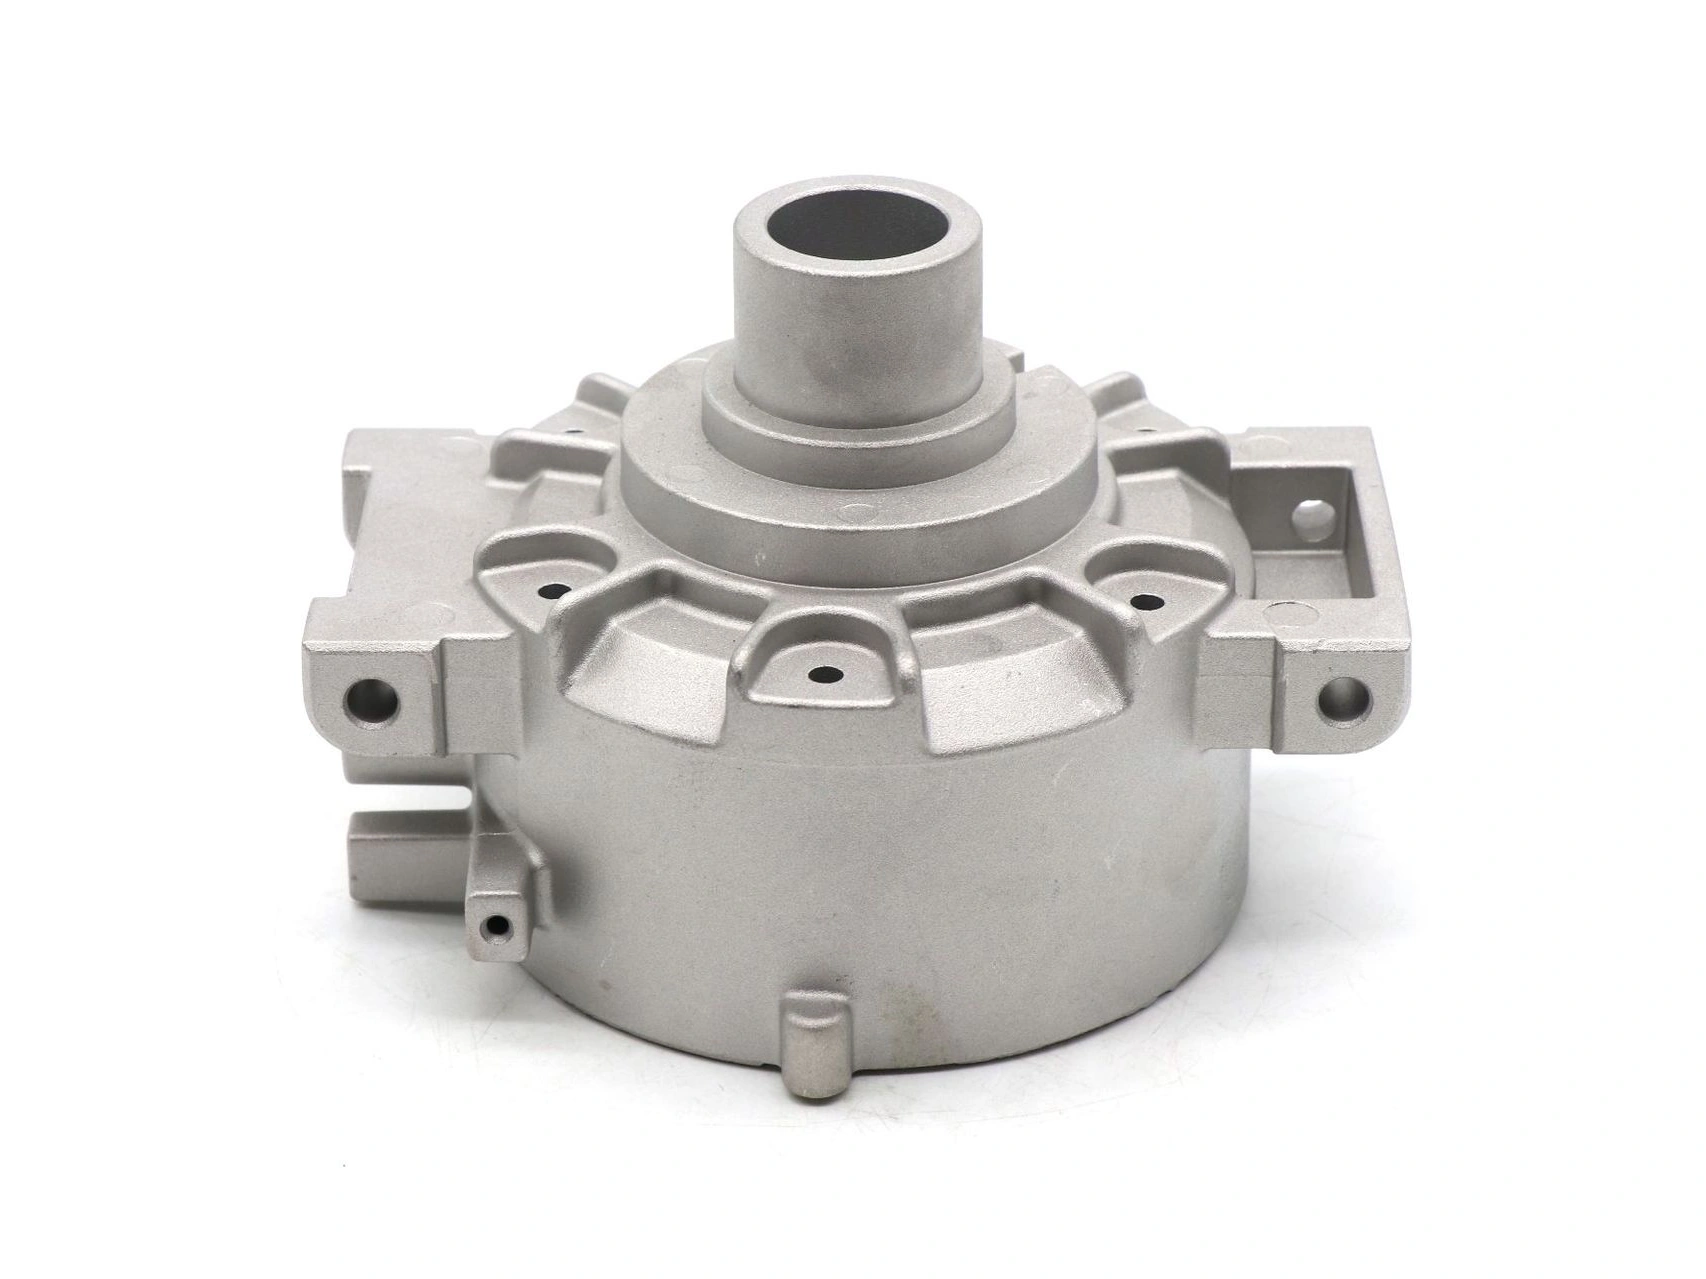
How Should Buyers Define Polishing Requirements for Aluminium Castings?
Buyers should define polishing requirements with a revision-controlled surface map, not a note saying "polish required." Mark cosmetic, hand-contact, preparation, functional and no-polish zones; state the intended result, edge and witness limits, final coating, viewing conditions, accept/reject samples, inspection stage, demand and packaging. The supplier should return a process by zone, access limitations and accepted-part cost assumptions.
Keep appearance and function separate. Grain, gloss, scratches, pits and waves need visual controls. Datums, sealing faces, bores, threads and electrical contacts need measurable dimensional, roughness, cleanliness or performance requirements. A surface may carry both sets, but neither should be inferred from the other.
Mark surface zones on the controlled data
Use a colour-coded 3D model or referenced 2D view to identify each class and its boundary. Include the assembled orientation because primary visibility may differ from the loose-part view. Mark permitted gate, ejector and parting witnesses, required blend footprints, brushing direction, no-polish areas and features that need masking.
Boundaries prevent an operator from feathering farther into an adjacent datum or hidden face. They also let suppliers estimate tool access and manual content. If a deep pocket or interrupted surface cannot be polished uniformly, resolve that limitation during DFM rather than at final inspection.
Define the starting surface and operation
State whether polishing begins after trimming, blasting, tumbling or CNC. Set incoming limits for flash, gate vestige, mismatch, scratches, die solder and exposed pores. Without a stable input, a fixed finishing route produces variable contour, cycle and appearance.
Distinguish deburring, edge breaking, gate blending, directional brushing, sanding and buffing. A drawing may specify the required outcome while the supplier controls proprietary abrasive grade and settings, but the process plan must identify the route that will be qualified. The polishing process overview can help procurement use consistent vocabulary.
Use the right acceptance control
Requirement | How to define it | Common mistake |
|---|---|---|
Cosmetic appearance | Zone, lighting, distance, angle, orientation, viewing time and limit samples | Using "good" or "smooth" without a comparison boundary |
Directional texture | Grain direction, starts/stops, transitions and allowable variation | Approving one flat coupon instead of the actual geometry |
Surface roughness | Parameter, cutoff/evaluation method, measurement direction and exact zone | Applying one Ra value as a complete cosmetic specification |
Edge condition | Loose-burr prohibition, permitted break/radius and protected adjacent features | Allowing uncontrolled rounding near fit or sealing areas |
Material removal | Protected features, minimum section or post-polish dimensional requirement | Assuming cosmetic work cannot change dimensions |
Cleanliness | Compound/media removal, washing, drying and residue check | Using brightness as evidence that the part is clean |
Connect polishing to machining and coating
Identify whether CNC occurs before or after cosmetic work and how the transition is blended. Precision faces should normally be protected from uncontrolled abrasion. Where a polished area meets a machined feature, define the boundary and inspect the final datum, size or sealing requirement. The CNC machining scope should be quoted separately from cosmetic polishing.
Name the final finish system and service environment. Buffing compounds or embedded media can affect cleaning and coating. High-gloss polishing may be unnecessary or counterproductive for a coating that needs a qualified surface profile. Approve the actual sequence through pretreatment, masking, coating, cure and final appearance.
Define defect and rework boundaries
List allowed process witnesses and cosmetic indications by zone. State that polishing cannot accept or repair cracks, cold shuts, shrinkage, oxide folds, pressure-path porosity or dimensional nonconformance. If local blending of superficial traces is allowed, define maximum area, depth or post-rework contour and the required reinspection.
Preserve traceability by tool cavity, polishing batch and coating batch. This separates a die mismatch from operator scratches or coating contamination. Repeated defects should trigger root-cause review, not an expanding rework allowance.
Control reference samples
Use physical accept and reject limit samples from production-intent castings. Label drawing revision, cavity, polishing route and final finish. Protect samples from oxidation, rubbing and contamination, and review them at defined intervals. Photos are useful for location and communication but can distort gloss, colour and fine texture.
Approve each relevant cavity and the complete downstream process. A hand-finished presentation sample can demonstrate an aesthetic direction, but it does not prove production repeatability or accepted unit cost. Record which changes require renewed sample approval.
RFQ checklist
Send revision-controlled CAD/drawing, assembled-view surface classes, starting-surface limits, operation outcome, no-polish features, edge requirements, limit samples, final finish, inspection and test stage, forecast, batch pattern and packaging. Ask suppliers to identify abrasive route, manual versus automated content, fixtures/masks, cleaning, subcontract operations, sampling, access exclusions and defect ownership.
The broader die-casting surface specification guide can support drawing notes. For commercial comparison, ensure every quote includes the same gate/parting blend, polishing, cleaning, coating, final visual inspection and packaging scope.
Production release and change control
Release production after representative castings from intended cavities pass post-polish dimensions, visual limits, cleanliness and the final coating or functional checks. Record tool revision, alloy, cavity, polishing work instruction and finish route. Trial evidence applies only to that identified combination.
Review changes to die surface, gate trim, cavity repair, abrasive/media, equipment, fixture, polishing location, cleaning supplier, coating route or packaging. Revalidation can focus on affected characteristics, but appearance should not drift through undocumented process substitutions.
Buyer decision
A publishable polishing requirement tells the supplier where, why, how and at what stage a surface is accepted. Zone the part, stabilise the incoming casting, separate visual and functional controls, approve production-intent limit samples and include the complete downstream finish. This definition supports accurate quotation and repeat production while preventing polishing from becoming an uncontrolled defect-hiding operation.