How do you ensure dimensional accuracy for high-tolerance components?
Dimensional accuracy for high-tolerance components is ensured by assigning each critical feature to the process that can control it, establishing functional datums, controlling tool and casting temperature, machining only where needed, and validating the measurement system before claiming capability. A tolerance is not guaranteed by a precise mold or CNC machine alone. Feature size, span, alloy, section changes, parting lines, moving cores, cavity, fixturing, coating, and measurement condition all contribute.
Separate functional characteristics from general dimensions
Start with the assembly. Identify bearing seats, sealing lands, fastener patterns, connector locations, gear or shaft relationships, and surfaces that locate the part. These characteristics deserve datum control and a planned manufacturing route. Non-mating exterior surfaces can usually use a tolerance appropriate to casting and appearance rather than inherit the tightest value on the drawing.
GD&T should express the relationship that protects function. Position may control a hole pattern more effectively than independent coordinate dimensions. Profile can control a complex mating surface. Flatness, perpendicularity, runout, or coaxiality should reference the part condition and datum setup that match assembly. A requirement that different inspectors interpret differently is not a stable control.
Allocate cast and machined features
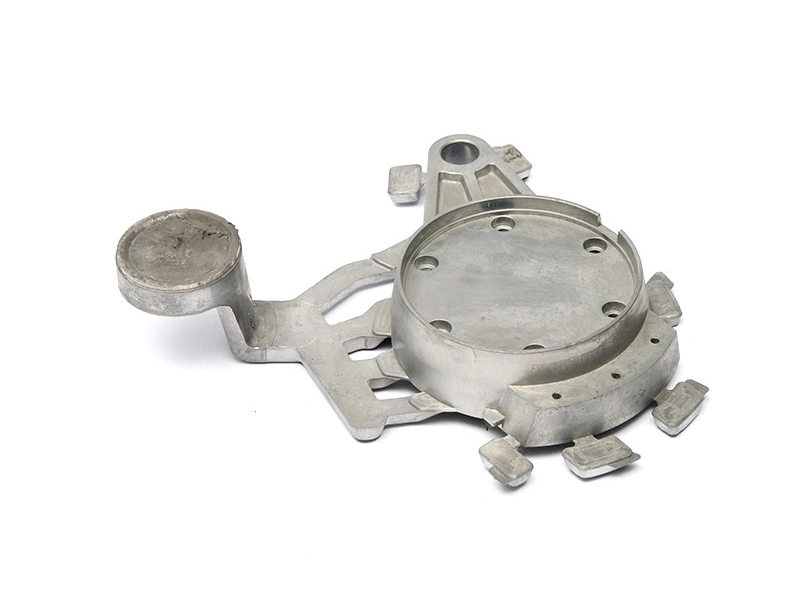
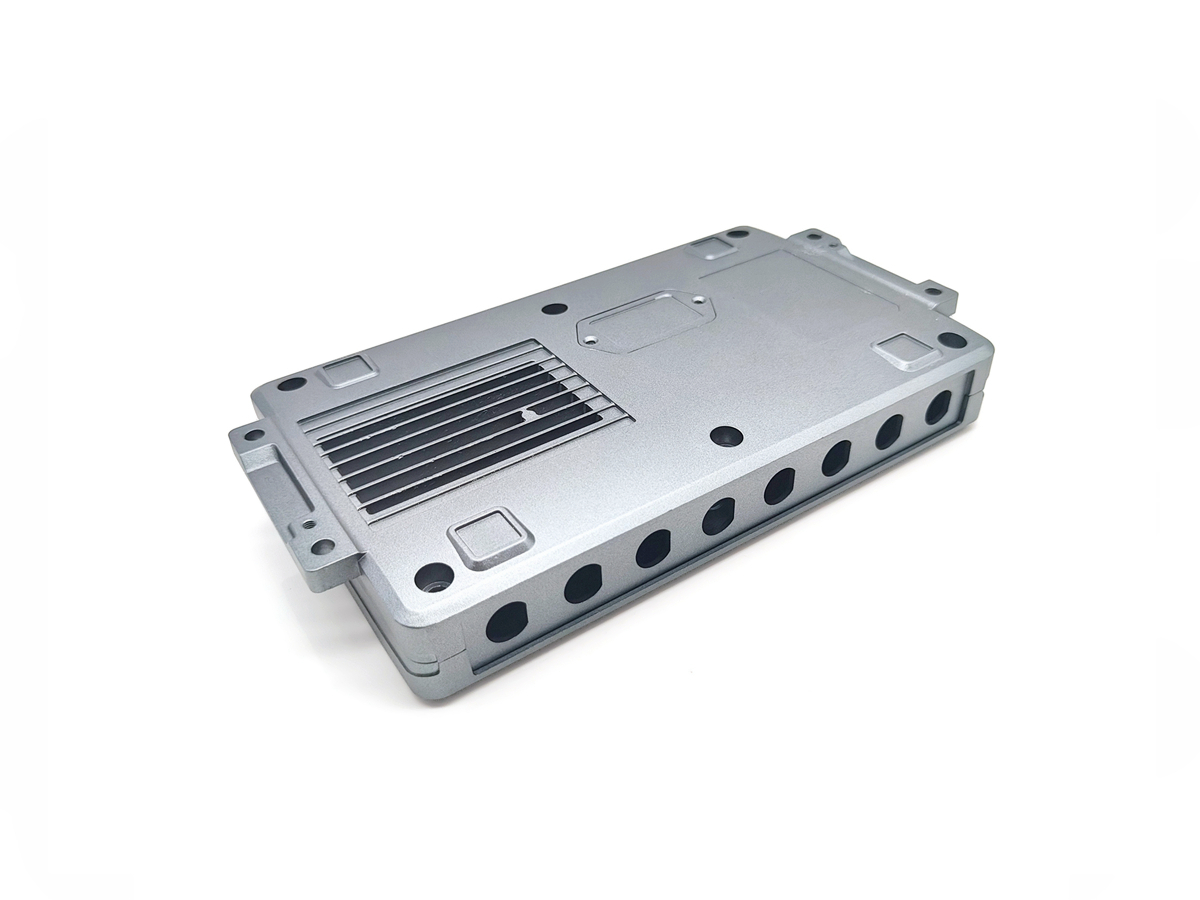
As-cast geometry is affected by tool construction, thermal contraction, ejection, section balance, and cavity differences. High-value interfaces that exceed the verified casting window can receive post-casting machining. This is not a reason to machine every surface. It is a deliberate allocation of precision to features that affect sealing, rotation, fit, or alignment.
Machining stock must account for casting variation without becoming so deep that it exposes unnecessary subsurface material. The raw casting needs stable locating points, and the operation sequence should create the primary machined datum before related features. Clamp force, tool wear, burrs, temperature, and release of residual stress can move a dimension even when the machine program is correct.
Accuracy risk | Control before production | Production evidence | Buyer decision |
|---|---|---|---|
Dimension crosses a parting line or moving core | Review tool alignment, lock, wear surfaces, and flash limit | Results by cavity and tool-maintenance records | Accept as cast, change datum, or machine |
Large thin surface has flatness requirement | Balance wall, cooling, ejection, stabilization, and restraint definition | Timed measurements in the specified free or restrained state | Revise geometry, fixture, or tolerance condition |
Machined bore must align to cast mounting points | Design raw locating scheme and stock around the bore | Fixture study, first-piece layout, ongoing gauge data | Approve datum transfer and machining route |
Coating affects a close fit | Define thickness, masking, racking, and measurement stage | Finished-part dimension and assembly check | Adjust allowance or keep the interface uncoated |
Control tooling and thermal balance
Precision begins with a maintainable tool concept. Cavity support, insert interfaces, slides, core pins, cooling, gates, vents, and ejectors can influence dimensions. The tool should include accessible reference features and replaceable wear elements where practical. Tool acceptance compares the manufactured cavity with the approved design, but casting trials determine how that cavity behaves thermally.
Uniform process conditions matter because alloy and die temperature affect fill, contraction, and release. A broad thin region and a heavy boss will not cool alike. Simulation and trial measurements can guide local cooling or cavity compensation, but one global shrink factor rarely predicts every dimension. Corrections should use stable-process data and account for the direction and feature involved.
Establish measurement before capability
A coordinate measuring machine, scanner, comparator, or gauge is useful only with a defined setup. Specify datum simulation, supports, clamp force, probe or optical access, alignment, filtering, temperature, and time after casting or machining. Flexible components can show different results in a free state and in an assembly fixture; the drawing and inspection method must state which one governs.
Run a measurement-system study suited to the feature and decision. Repeatability, reproducibility, resolution, fixture variation, and correlation between methods should be understood before process spread is calculated. Scanning a complex profile and gauging an assembly interface may both be appropriate, but they do not automatically produce interchangeable results.
Use trials to close the control loop
First tool samples establish a stable casting condition before dimensional correction. Measure all cavities separately, review fill and ejection, then perform a layout from the approved datum scheme. After tool correction, repeat the layout on new samples. Machine and finish representative parts because those operations can change both dimensions and measurement access.
Capability evidence should identify the exact feature, cavity, material, process state, sample plan, and measurement method. If the process cannot hold a requirement, options include changing geometry, revising the tolerance to match function, adding machining, changing the datum or fixture, or selecting another process. The decision should occur before mass production, not after rejected assemblies accumulate.
Information needed for a tolerance review
Provide the controlled 3D model and drawing, mating parts, datum intent, critical-to-quality list, assembly and gauge conditions, material and casting route, annual volume, machining and coating plan, and any existing measurement data. Mark dimensions that are regulatory or functionally fixed and those open to alternative control.
The achievable tolerance can then be confirmed feature by feature through DFM, tool trials, metrology, and capability evidence. Without geometry, process, cavity, fixture, and measurement context, a universal high-tolerance number is not a reliable basis for quotation or acceptance.