What materials can urethane casting simulate for functional testing?
Urethane casting can simulate selected attributes associated with rigid plastics, flexible elastomers, clear plastics and soft-touch overmolds, but it should not be specified as an exact substitute for ABS, PP, PC, nylon, PEEK, TPE, silicone or metal. Choose the polyurethane from the functional test: stiffness, hardness, impact response, flexibility, clarity or tactile feel. Then verify that attribute under the actual load, environment, duration and part geometry.
Select an Attribute, Not a Material Name
| Testing need | Cast attribute to screen | Evidence | Boundary |
|---|---|---|---|
| Housing assembly | Stiffness and local deflection | Mating trial and measured load/deflection | Does not prove production creep or molded orientation |
| Latch or clip concept | Short-term flexibility and recovery | Defined actuation and cycle screen | Does not qualify production fatigue life |
| Grip or button | Hardness, section response and tactile friction | User task plus identified variants | Does not establish long-term compression set |
| Clear window or flow model | Clarity, tint and visible bubble level | Physical reference and optical viewing condition | Does not prove UV or production optical performance |
| Seal concept | Compression, recovery and interface geometry | Leak or compression test at stated conditions | Fluid aging and service life remain material-specific |
Rigid Plastic-Like Prototypes
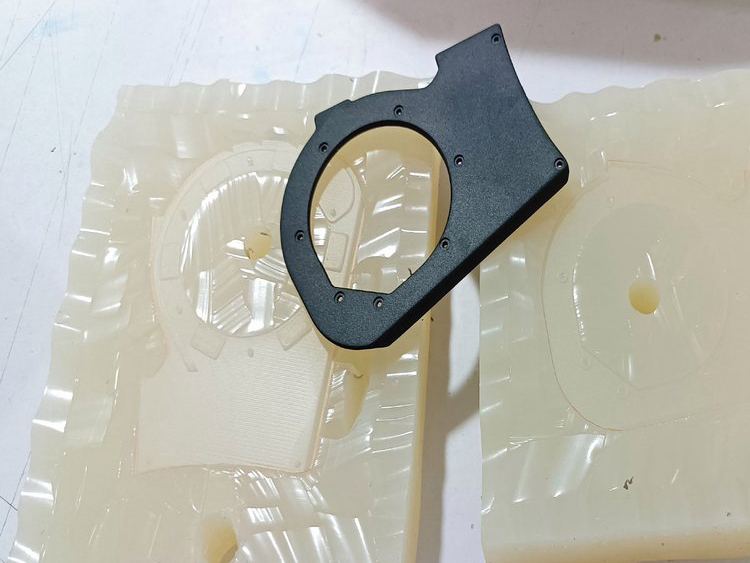
Rigid polyurethane systems can be selected for housings, bezels, covers, brackets and internal carriers when the team needs assembly stiffness, handling or a short-term load screen. The useful comparison may be local deflection around a boss, whether a cover stays seated, or how a wall feels during use.
A production thermoplastic's response depends on its grade, additives, moisture, molding history, orientation and section. A cast material with similar room-temperature stiffness can differ in impact fracture, creep, thermal response and chemical exposure. State which response matters and test representative sections. Do not approve a production resin from a generic "ABS-like" description.
Flexible and Elastomer-Like Prototypes
Flexible polyurethane can support grip, bumper, button, bellows and gasket concepts. Hardness is only one input. Thickness, support, strain rate, temperature, texture and the loading direction affect what a user feels and what a fixture measures.
Specify the desired function: comfort, travel, rebound, impact cushioning, retention or sealing. Compare identified material variants in the same geometry and condition. For cyclic or environmental requirements, use the cast result to narrow the design, then test the specified production elastomer. Polyurethane chemistry should not be assumed to duplicate silicone rubber, TPE or another elastomer across wear, tear, compression set and fluid resistance.
Clear and Translucent Prototypes
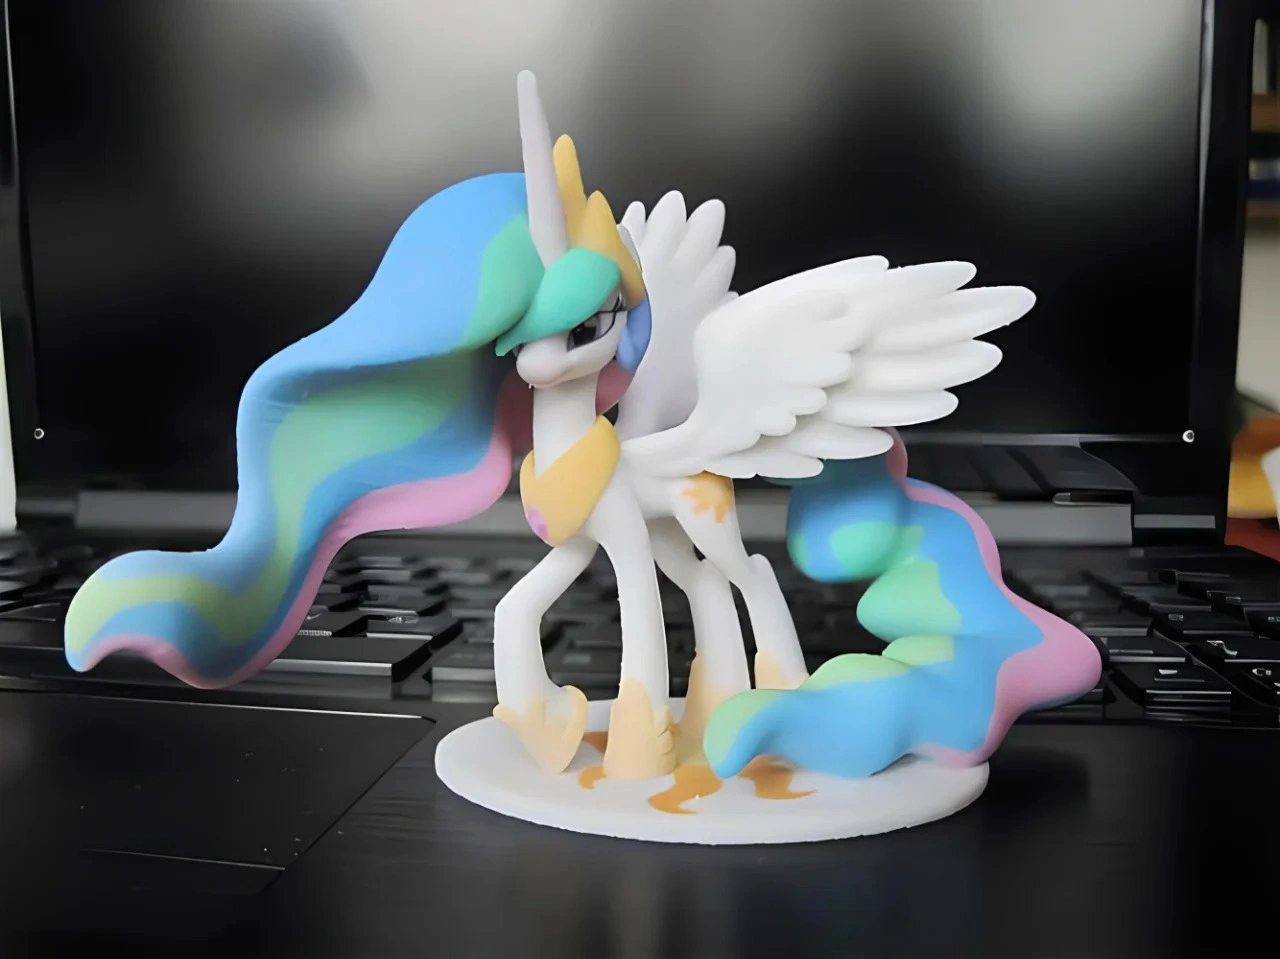
Clear or tinted castings can make internal routing visible, support light-pipe concepts or provide an appearance sample. The master surface, mold clarity, resin handling, bubbles, wall thickness and post-finishing all affect the result. A polished outer surface cannot correct a void or flow mark inside the wall.
Define whether the requirement is visual access, tint, haze, distortion or light transmission. Approve a physical reference under controlled lighting and viewing distance. If internal bubbles could affect a fluid path or optical measurement, specify inspection accordingly. Long-term UV, yellowing and production optical performance remain open until evaluated in the actual material and process.
Multi-Material and Soft-Touch Zones
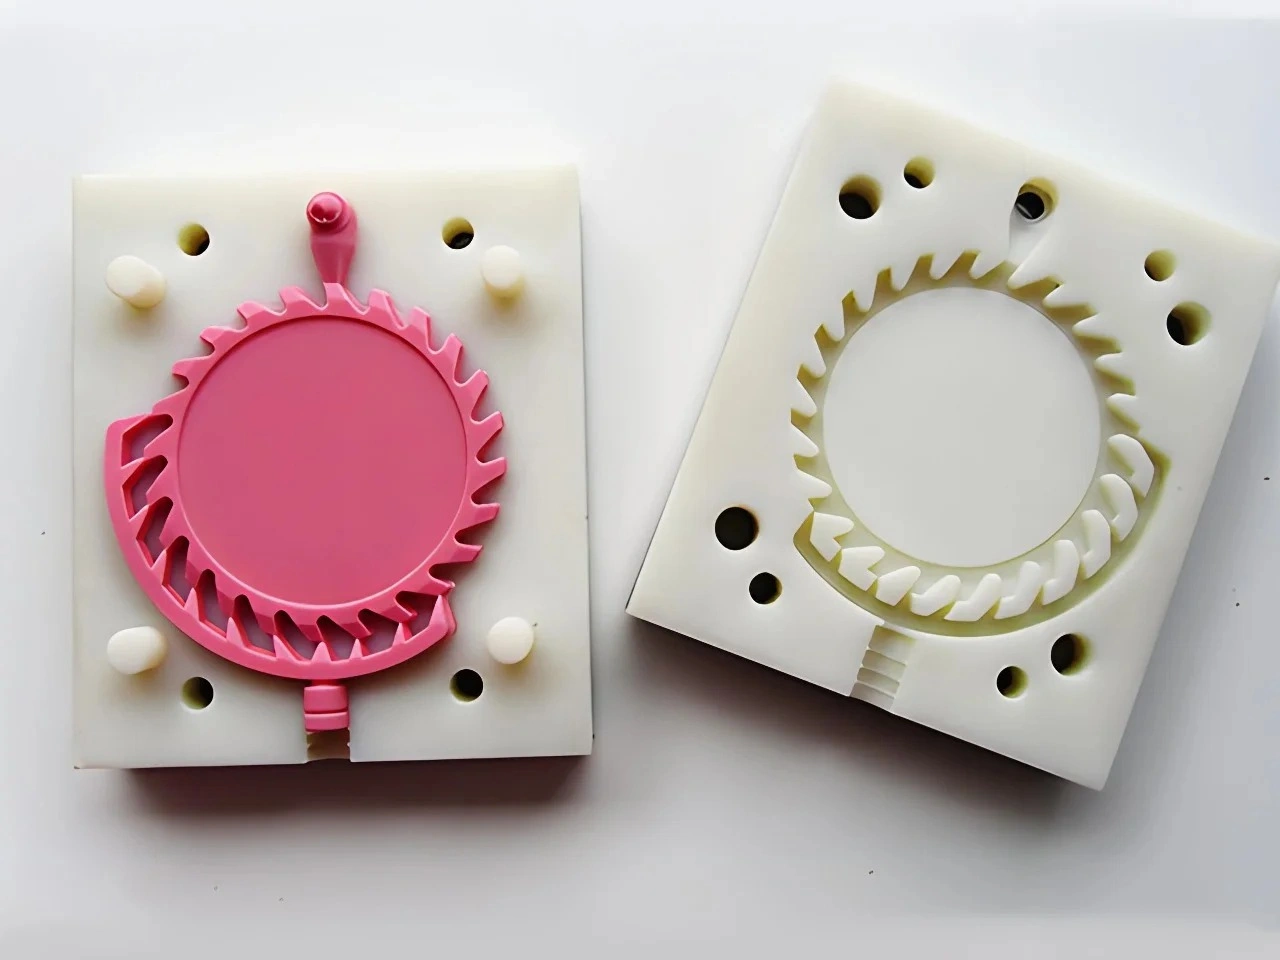
Sequential casting can combine rigid and flexible polyurethane regions, and inserts can be cast into the part. This helps evaluate interface coverage, tactile position, overlap, mechanical keys and insert access. Separate cast parts may be better when variants need rapid swapping or the intended product is assembled rather than overmolded.
Bonding depends on resin chemistry, cure state, surface preparation, contamination and geometry. Define whether the interface is cosmetic, load-bearing or sealing. Section sacrificial samples and use pull, peel, torque or leak tests where relevant. Cast adhesion does not qualify production thermoplastic overmolding.
Metal-Like Appearance Is Not Metal Performance
A filled resin or metallic finish may create weight, color or surface cues for a demonstration, but it does not simulate metal conductivity, stiffness, yield, fatigue, shielding or high-temperature behavior. If a project question depends on aluminum, zinc, copper alloy or steel performance, use an appropriate metal prototype or production-intent process.
Be explicit when a polyurethane shape represents only the envelope of a future metal component. This protects test conclusions and prevents stakeholders from treating appearance as structural evidence.
Write the Functional Test Before Selecting Resin
State load mode and magnitude, support points, temperature, fluids, UV or humidity exposure, duration, impact location, cycle count and pass/fail criterion. Identify which results are comparative and which are absolute. Ask the supplier for the candidate material designation, available data and relevant cure/conditioning procedure.
Test samples of known age and history. Preserve failures and inspect fracture or interface surfaces. If a full-part result combines geometry and material effects, use a coupon or simplified feature to isolate the property. The material-simulation decision guide gives additional screening categories.
Buyer Material RFQ
Send production material and process for context, but separately state the cast prototype's target attribute. Include part geometry, section, color or clarity target, environmental condition, test method, sample quantity and data/report needs. Request material identity and traceability appropriate to the decision.
The purpose of urethane material simulation is to reduce a design space with evidence. It is not to relabel polyurethane as a production polymer. The urethane casting service overview describes the broader process; final production qualification must use the specified production material and manufacturing route.