Diecast Foundry Selection: Alloy Control, Casting Practice and Traceability
A diecast foundry should be selected by its ability to control the complete route from alloy charge and tool condition to trimmed, machined, finished, and inspected parts. Equipment capacity matters, but it does not answer whether the foundry can hold the part's critical interfaces, manage porosity risk, maintain vents and cooling, or trace a change to a specific lot. Start with the drawing, alloy, geometry, quantity, and acceptance plan. Then ask the foundry to show how its process addresses the actual features.
Die casting is sensitive to the relationship between metal temperature, die temperature, filling, pressure, venting, cooling, ejection, trimming, and maintenance. The same nominal machine can produce different results with a different tool, alloy, wall layout, or cycle. A sound qualification therefore combines a DFM review, tool trial, feature-based inspection, material evidence, and a production record. It does not rely on a generic machine tonnage or a claim that every alloy follows the same route.
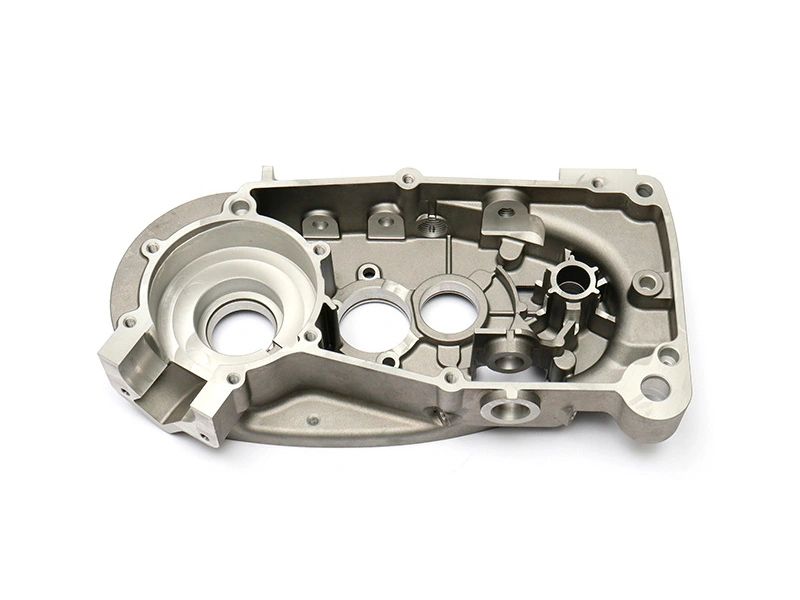
Alloy Control Starts Before the Furnace
The foundry should know which designation controls, how the charge material is identified, which additions are allowed, and how the melt is associated with the casting lot. The buyer should state chemistry, condition, restricted elements, certificate requirements, and any customer-specific material rule. If the supplier uses returns or blends material, the method should be controlled and documented within the applicable specification. A certificate is useful when it can be traced to the parts and when its scope is understood.
Material selection also affects tool and process decisions. Aluminum, zinc, magnesium, and copper alloys create different concerns for die wear, thermal cycling, filling, machining, and finish. An alloy alternative should be reviewed against the requirement that caused the original selection. A different grade may change corrosion, strength, conductivity, wear, plating response, or pressure integrity. The buyer should require a technical comparison and approval rather than accepting a similar trade name.
Use Material Evidence Without Overreading It
Material evidence confirms identity within its stated scope. It does not prove that every casting is free from porosity, that a machined pressure boundary will pass, or that a surface finish will meet appearance expectations. Those questions need process and finished-part evidence. Keep the material record linked to the tool, lot, machining, finish, and test records. If a material result is outside the requirement, contain the associated parts before a visual or dimensional pass allows them to move forward.
Molding Practice Is Visible in the Part
Die design and molding practice should be reviewed together. Parting lines, slides, cores, gates, runners, vents, overflows, cooling channels, and ejectors determine how metal reaches and leaves the cavity. The foundry should mark the sensitive areas on the drawing and explain how the tool supports them. A remote corner may need a different fill strategy from a thick boss; a cosmetic face may need a different parting and trimming decision from a hidden mounting pad.
Tool condition changes over time. A worn shutoff may create flash, a damaged gate may change filling, a blocked vent may trap gas, and a cooling restriction may move dimensions or surface condition. The foundry's maintenance record should identify the tool area, measured condition, repair, and reapproval check. If the tool is run by different shifts or moved between machines, the buyer should understand how the approved process settings and tool identity remain controlled.
Read the Trial Against Feature Risk
A tool trial should review thin areas, heavy sections, remote corners, slides, shutoffs, ejection marks, parting mismatch, and trimming access. Follow the casting through cleaning and machining because a rough sample may not reveal how stock removal affects a bore, seal, or wall. Record the tool revision, alloy lot, machine or process state, and inspection method. If the trial is exploratory, label it as such; do not confuse feasibility evidence with final production approval.
| Foundry control point | Part symptom when unstable | Evidence for qualification |
|---|---|---|
| Alloy charge and melt identity | Chemistry variation or untraceable lot | Material record linked to heat, melt, or casting lot |
| Vent and overflow condition | Trapped gas, cold fill, flash, or inconsistent surface | Tool inspection, trial notes, and defined visual or internal checks |
| Cooling and cycle control | Distortion, dimensional movement, or local surface change | Process record and feature-based dimensional results |
| Tool maintenance | Flash, shifted holes, worn edges, or repeated repair defects | Tool history, repair record, and reinspection |
| Trim and machining handoff | Damaged interfaces or exposed casting condition | Finished-part report and agreed datum or test state |
Traceability Should Support Containment, Not Just Paperwork
Traceability is useful when a part mark or lot code leads to the material, tool, machine, shift or run, machining, finish, inspection, and packaging records. The mark should be placed where it does not affect the assembly or appearance. Define how the foundry contains parts when a defect is found after machining or customer assembly. If the code cannot distinguish tool cavities, shifts, or process changes where they matter, the buyer may need a stronger identification rule.
Subcontracted operations need the same discipline. If machining, plating, painting, tumbling, or testing is performed outside the foundry, the primary supplier should retain responsibility for the lot relationship and nonconformance response. Ask who controls the specification at the subcontractor and how a changed process is approved. A casting can pass at the foundry and fail after a poorly controlled finish or machining operation.
Quality Records Need a Defined Retention and Review Scope
Agree which records are provided with samples, which accompany each lot, and which are retained for investigation. The buyer may need material certificates, dimensional reports, leak or pressure results, surface or finish records, tool trial reports, and deviations. The requirement should identify sample quantity or lot basis where relevant and should not request a document without a decision attached to it. Records are valuable when they show the part state, revision, equipment, datum, and acceptance rule.
Use an RFQ and Technical Review to Test Foundry Fit
Provide the drawing and model, alloy, quantity, casting route, finished state, cosmetic areas, machined features, inspection, packaging, and change rules. Ask for a marked-up DFM review, tool concept, gate and vent approach, maintenance assumptions, trial plan, material evidence, and subcontracting list. A technical call or site review should follow the same checklist. The purpose is to see whether the foundry explains the part in process terms, not simply whether it has a large machine.
Neway's metal casting route can be considered when a buyer needs the casting process connected with tooling, machining, and quality records. Ask for clear boundaries around what is included and what depends on the final drawing, alloy, volume, and test plan.
Connect Foundry Records to the Actual Process State
A diecast foundry's process record should identify the material lot, tool or cavity, machine or cell, process revision, and relevant inspection state. The record does not need to expose every internal control parameter to be useful. It does need to show that the shipped parts came from the approved route and to make a later investigation possible. If the part is machined or finished after casting, the record should follow the identifier through those operations.
Incoming material, melt preparation, casting, trimming, cleaning, machining, finishing, testing, and packing each create a possible change. The foundry should define what is recorded at each handoff and how a nonconforming result stops or contains the affected lot. A material certificate with no part relationship is weak traceability. A dimensional report with no tool or datum identity is difficult to reproduce.
Ask How the Foundry Controls Process Drift
Process drift can come from tool wear, vent blockage, cooling restriction, alloy change, machine setup, fixture movement, or a changed finishing step. The foundry should explain which observations trigger a review and how the process is returned to the approved condition. For example, flash may lead to a tool inspection, a shifted hole may lead to a slide or core check, and a surface change may lead to a vent, fill, or cleaning review. The response should connect the symptom to the responsible operation.
Do not require a fixed capability number without a defined part and measurement method. A useful control plan identifies the feature, datum, equipment, sample basis, and reaction when the result changes. Neway's tool and die making route can be included when tool condition and casting consistency need one owner.
Tool Maintenance Is Part of Foundry Qualification
Die casting tools combine cavity surfaces with gates, runners, vents, overflows, slides, cores, ejectors, cooling passages, and inserts. Each area wears or accumulates residue differently. The foundry should show how these areas are identified, cleaned, inspected, and repaired. A tool maintenance record should state the location, observed condition, action, and post-maintenance check. This gives the buyer a way to relate a part defect to a specific tool event.
Cooling and vent access are practical qualification points. A passage that cannot be flushed or checked may become a hidden source of drift. A vent that is inaccessible may be cleaned inconsistently. A slide that has no repeatable locating reference may be repaired into a different position. The tool review should include access, spare parts, insert strategy, and the approval path after a repair.
Audit the Casting-to-Machining Handoff
Machining can expose a casting condition that was not visible on the outside. A bore may open a void, a face may reveal a lap, or a thread may intersect a defect or core shift. The foundry and machining team should agree the raw datum, stock, fixture support, and finished acceptance state. If machining is subcontracted, the primary supplier should control the revision, part identity, and nonconformance response.
Neway's post-machining route can be reviewed with the foundry process so that raw-casting evidence is not mistaken for finished-part evidence. For a pressure or sealing feature, specify whether the test is run before or after machining and finishing. For a cosmetic face, inspect after the complete clean and finish sequence.
Separate Foundry Qualification From Production Monitoring
Qualification proves that a proposed route can make the part under an agreed condition. Production monitoring checks that the approved route remains in place. The two stages may use different sample quantities and records, but they should share the same part revision, tool identity, material requirement, and acceptance logic. An early trial can identify a design change; a production check should not silently accept that change as the new baseline.
During qualification, review the raw casting, trim, machining, finish, and inspection states. During production, monitor the features that reveal drift and retain the records needed for containment. The monitoring plan should be proportional to the consequence of failure. A rough nonfunctional exterior may need visual control, while a machined pressure boundary may need a defined leak test or other evidence.
Control Subcontracted Finishing and Testing
Subcontracting can be practical, but it creates a handoff that should be visible. Identify who owns the drawing revision, material or coating requirement, sample approval, packaging, and corrective action. Keep the cast lot linked to the machined, plated, painted, tumbled, or tested result. If a subcontractor changes its process, the primary supplier should determine whether the approved part or inspection method is affected.
Finish and cleaning can influence dimensional fit and appearance. A coating may enter a thread or bore; tumbling may alter an edge; blasting may change texture; and washing may leave residue if drainage is poor. The foundry qualification should inspect the part in the state delivered to the buyer. Neway's post-process route can be reviewed where surface treatment forms part of the diecast component.
RFQ Inputs for a Diecast Foundry
Provide the drawing and model, alloy, quantity, machine or process constraint if known, cosmetic zones, functional datums, machined features, pressure or environmental requirement, finish, inspection, packaging, and required records. Ask the foundry to state tool concept, material traceability, maintenance, trial evidence, subcontracting, and change control. If the part will be quoted as an assembled product, identify the supplied hardware and the final assembly test.
Neway's casting material route can be considered with the foundry scope when alloy identity and process records need to stay connected. The buyer should approve the route based on the actual product and evidence rather than the name of the equipment.
Check the Material Source and Production Handoff
A diecast foundry should be able to explain where alloy or charge material enters the process and how it remains associated with the casting lot. If material comes from several sources, identify the approved sources and the evidence used to release them. If returns or additions are used, the control method should remain within the applicable material specification.
The handoff from melt to casting should preserve the lot identity. A material certificate that cannot be connected to the castings is difficult to use in a complaint. The same principle applies when the part moves to trimming, machining, finish, testing, or packing. Neway's casting material route can be reviewed with the foundry's traceability plan.
Review Process Changes Against the Approved Sample
A tool repair, vent cleaning method, cooling connection, machine change, alloy source, or finish subcontractor can affect the part. The foundry should record the change, identify the affected feature, and decide whether the approved sample or inspection plan still applies. This does not require repeating every test for every routine action; it requires a reasoned link between the change and the risk.
Surface Quality Starts With the Tool and Ends With Handling
Parting witness, gate cleanup, flash, ejector marks, texture, and handling damage can affect appearance and assembly. Review the tool surface, trim process, cleaning, mass finishing, coating, and packaging as a chain. A coating may hide a mark but not repair an unstable edge or poor substrate. A clean part may still be scratched by a hard separator.
Neway's post-process route can be evaluated with the foundry process when a finished surface is part of the purchase. The sample should use the same casting, cleaning, and finish condition that production will deliver.
Validate Functional Features in the Finished State
A diecast foundry may inspect a raw part, but the buyer should decide whether the functional requirement exists before or after machining. A bore, thread, seal, pressure wall, or locating pad often becomes meaningful only after the downstream operation. Define the datum, fixture, test, and finished state. This prevents an external dimension report from being mistaken for proof of a finished assembly.
If a test is outsourced, identify the test laboratory or process owner, sample identity, method, and result. The primary supplier should retain the relationship between the test and the casting lot. If an item fails, preserve the raw and finished samples where practical.
Questions for a Foundry Technical Review
Ask how the foundry controls alloy identity, tool revision, vent and cooling condition, core or slide location, ejection, trim, cleaning, machining, finish, inspection, nonconformance, and change. Ask for examples of the records used, not for unsupported performance figures. The review should follow one part from material receipt to packaging so handoff gaps are visible.
Buyer Summary
A suitable diecast foundry controls material identity, tool and molding practice, maintenance, downstream operations, inspection, and traceability as one route. Equipment capacity is only one part of that decision.
Qualify the foundry against the actual part features and the evidence needed to approve them. That gives purchasing a defensible comparison and gives engineering a clear path for production changes.
FAQ