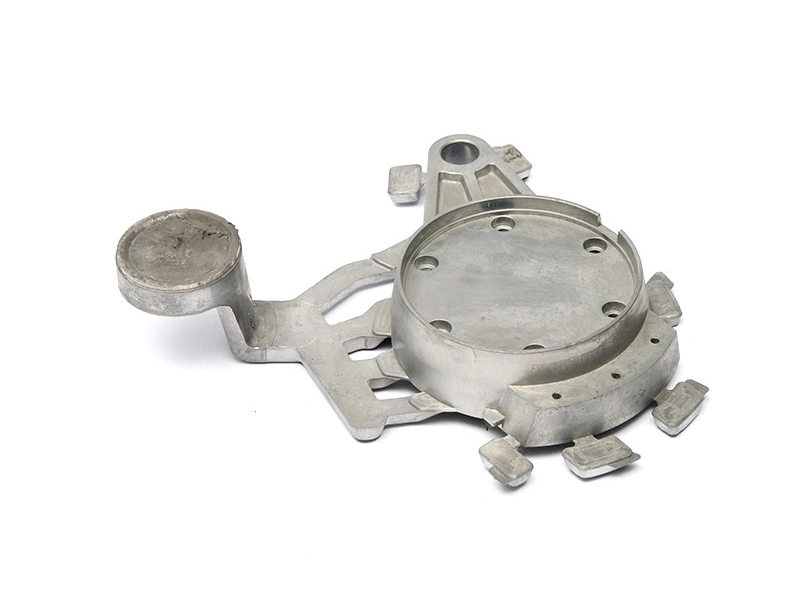
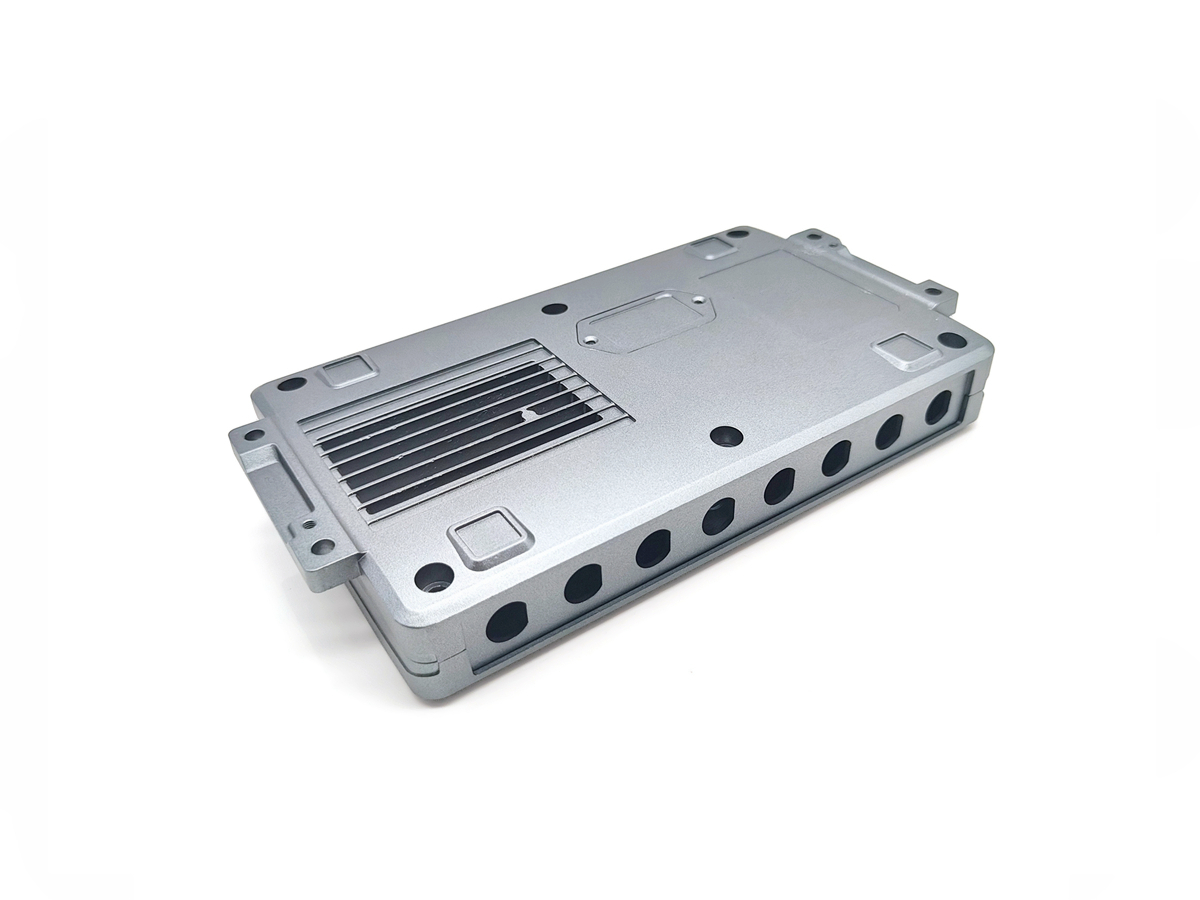
What is Low-Pressure Die Casting?
Low-pressure die casting (LPDC) fills a reusable die by applying controlled gas pressure above molten metal in a sealed furnace, pushing the metal upward through a riser tube into the cavity. Pressure is maintained while the casting solidifies so liquid metal can continue feeding regions connected to the gate. It is commonly considered for aluminum parts that need controlled filling and sound load-bearing sections, but suitability depends on alloy, geometry, feeding path, volume and required evidence.
How the LPDC system works
The furnace sits below or adjacent to the die and remains connected through the riser. A programmed pressure curve raises metal into the die without the high gate velocity associated with high-pressure die casting. After fill, the pressure profile supports feeding as solidification progresses. When the gate has frozen sufficiently, pressure is released and unfrozen metal in the riser can return to the furnace before the die opens.
This architecture is the defining relationship: furnace pressure controls metal rise, the bottom gate establishes the feeding route, and die cooling establishes the solidification sequence. Calling any low-velocity permanent-mold process LPDC misses those relationships. The supplier should show how its equipment measures and controls the pressure response and thermal state for the proposed part.
Where LPDC can be a good fit
LPDC is often evaluated for wheels, suspension-related structures, housings and other aluminum parts with substantial load paths or pressure-integrity concerns. The process can fill with less free-surface turbulence than a very fast injection route, and pressure feeding can support soundness in connected regions. Those are process tendencies, not automatic guarantees of low porosity or superior strength.
A good candidate has a geometry that can be gated and directionally solidified from the lower feed path. The die must accommodate cores, ejectors and cooling while keeping critical regions connected to feed metal. Isolated heavy junctions, blind pockets, long thin extremities and abrupt section changes may still create shrinkage, oxide or incomplete-fill risk.
Compare LPDC with other routes
Decision | LPDC tendency | Route to compare | Evidence needed |
|---|---|---|---|
Metal filling | Controlled upward rise from a sealed furnace | Gravity permanent mold or HPDC | Fill study, trial sections and defect locations |
Production rate | Solidification and pressure sequence can govern cycle | HPDC for high-rate complex parts | Stable accepted output at forecast demand |
Feeding | Pressure can feed regions connected to the gate | Gravity casting with risers | Solidification review and internal inspection |
Tool economics | Reusable metal die and dedicated process hardware | Sand casting for uncertain lower volume | Tooling, cycle, yield and lifetime-volume model |
HPDC may be more economical when very fast cycles, intricate thin walls and extensive feature integration dominate. Gravity or sand casting may be better when tooling flexibility, very low volume or large section feeding controls the project. Compare the complete route under one acceptance plan rather than ranking processes by pressure level alone. The broader metal casting process review should occur before detailed tooling.
Alloy and melt quality
The selected aluminum grade must be suitable for the required casting route and final properties. Chemistry, hydrogen control, oxide management, furnace practice and transfer cleanliness affect internal quality. The enclosed furnace can reduce some exposure during filling, but it does not remove inclusions already present or correct poor melt control.
Ask whether properties will be accepted from material certificates, separately cast specimens or representative casting locations. Heat treatment, if specified, must be qualified with the actual alloy and casting condition. Do not transfer values from a different process or product form without engineering justification.
Tooling and thermal design
Gate position, die cooling and local insulation must establish a feedable solidification path. A region that freezes between the gate and a heavy section can cut off feeding even while furnace pressure remains applied. Cooling channels should control critical junctions without freezing the gate prematurely. Core design must also allow venting, extraction and dimensional stability.
Simulation can compare fill and solidification concepts, but its boundary conditions need trial confirmation. Thermocouples, sectioning, density evaluation, radiography or mechanical testing may be appropriate depending on the risk. Use engineering review to connect model predictions to measurable acceptance.
Typical defects and process signals
Incomplete fill can result from insufficient metal head, restricted flow, heat loss or an unsuitable pressure rise. Oxide films can come from melt handling or turbulence. Shrinkage can occur where solidification loses contact with feed metal. Gas porosity, die erosion, distortion and surface laps remain possible. No single inspection method detects all of these conditions.
Monitor the pressure curve, furnace metal level, metal and die thermal state, cooling flow, cycle interruptions and cavity-specific defect locations. A stable command signal is not enough if the delivered pressure or metal level changes. Process records should be traceable to the sampled castings used for qualification.
What buyers should send
Provide controlled CAD and drawings, alloy, annual and lifetime volume, loads, pressure or leak duty, thermal history, heat-treatment requirement, corrosion exposure, machined zones and internal-quality limits. Identify functional datums, heavy junctions, sealing paths and failure consequences. State the required test method and sampling rather than requesting generally high integrity.
Ask the supplier for the proposed gate and feed route, die thermal concept, cores, process-monitoring plan, trim and machining routing, validation samples and cost assumptions. Compare LPDC against the strongest alternative using tooling, accepted cycle, yield, secondary work and inspection. LPDC is the right answer when its controlled upward fill and pressure-fed solidification solve the part's actual risks at the forecast volume, not merely because the process name sounds more precise.