Why is zinc die casting suitable for locks, handles, and hardware products?
Zinc die casting is suitable for many locks, handles and hardware products because it can combine compact mechanism features, ergonomic contours, stable hole spacing and a decorative finish base in one high-volume casting. It is not automatically secure, wear resistant or outdoor durable. The lock load path, handle abuse case, fastener interface, mating wear pair and complete plating or coating system must be designed and tested for the product.
Separate three hardware functions
Hardware function | Typical zinc value | Failure mode | Release evidence |
|---|---|---|---|
Lock or latch mechanism | Pivots, stops, spring pockets and keying in compact space | Wear, impact, burr interference and deformation | Loaded cycle with actual mating parts and contamination |
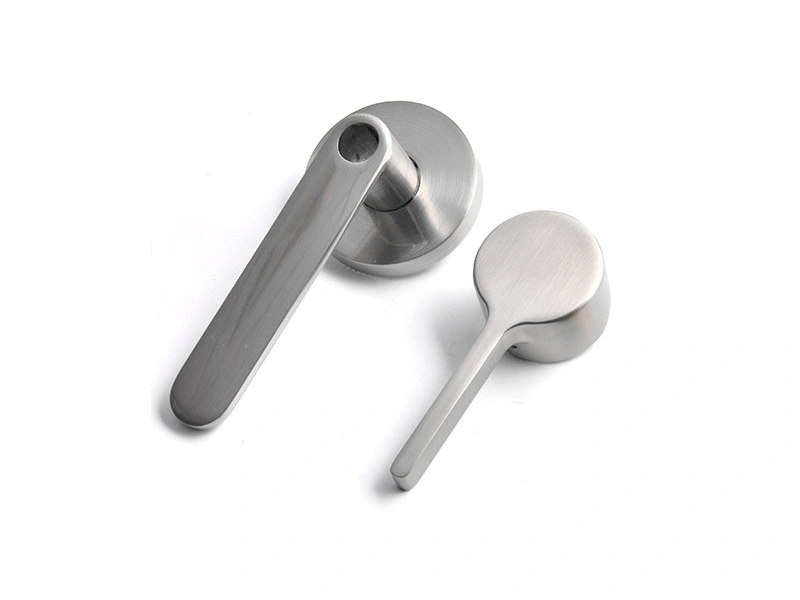
Handle or lever structure | Ergonomic form, bosses and attachment features | Bending, pull-off, boss damage and installation torque | Proof/abuse load, torque and repeated operation |
Decorative escutcheon or fitting | Crisp contour, logos and plated or coated visible face | Pits, waves, chips, cleaner attack and rack marks | Limit sample, adhesion, abrasion and exposure |
One product may combine all three functions. Mark structural, moving, fastening and cosmetic zones separately so a visual repair does not alter a load-bearing or mating feature.
Locks need mechanism-specific evidence
A lock body can integrate guide walls, cylinder supports, spring seats, screw bosses and cover alignment. A latch or cam can integrate stops and engagement contours. Zinc's feature density can reduce stamped pieces and fixtures, but flash or mismatch near a moving path can stop the mechanism.
Test with the production key, cylinder, springs, fasteners and mating strike. Include expected side load, misalignment, dirt and temperature. Security classification, if required, belongs to the complete lock standard and assembly; the zinc casting itself does not carry a security rating.
Handles need load and fastener control
Handle geometry should transfer user load into the mounting pattern without concentrating stress at a thin boss root or sharp corner. Define pull, push, bending, torsion and foreseeable abuse. For a lever, include the maximum offset load and return mechanism. A desired heavy feel may favor zinc, while a strict door or product mass target may not.
Installation torque deserves its own limit. Excess torque can strip threads, crack a boss or crush a coating; low torque can permit movement that damages the finish. Use the actual screw, washer, substrate and tool. Repeat removal if the product is serviceable.
Wear pairs need real mating parts
Zinc against steel, polymer, plated zinc or another material will not show the same friction and wear. Define contact pressure, motion, lubrication and contamination. Inspect play, force, surface loss and debris after cycling. A coating may reduce initial friction but wear through at an edge.
If a pivot or thread requires longer service than the base geometry can support, consider a pin, insert, bushing or selective machining. Feature consolidation should not eliminate replaceable wear elements that make maintenance practical.
Decorative finish starts with the casting
Polished plating can provide metallic appearance, while powder or paint can provide color and barrier protection. None hides cracks, cold shuts, deep sink or uncontrolled parting mismatch. Polishing may open subsurface pores and round lettering. Layer build can reduce thread or spindle clearance.
Specify primary and secondary visible zones, finish stack, permitted rack marks, viewing conditions and approved limits. Test abrasion at touch areas and corrosion at edges, screw seats and chips. The zinc finishing route should be approved on the complete hardware part.
Outdoor and wet hardware needs exposure detail
Rain, chloride, bathroom cleaner, perspiration, condensation and ultraviolet exposure create different coating demands. State orientation, wet/dry cycles, contact metals, cleaning and damage. A test duration is an acceptance condition, not a universal field-life conversion.
Watch crevices behind escutcheons, drainage around screws and galvanic contact with steel or aluminum. Check adhesion and operation after exposure because corrosion product or blistering can affect a moving mechanism before the base casting loses structural section.
Tolerance chains run through the assembly
Lock engagement and handle feel depend on more than casting size. Include spindle, cylinder, rose, door or cabinet thickness, fastener, gasket and mating strike in the stack. Dimensions within one die half may be repeatable while a slide-formed bore, polished face or plated fit carries more variation.
Use functional fixtures that represent the mounting product and verify operating force, free play and return. Measure final-state parts by cavity. If selective machining is needed, define its datum from the installed function rather than an easy as-cast surface.
Packaging protects the approved finish
Handles and decorative fittings can scratch each other, polish through a coating at contact points or stain when trapped moisture reaches the package. Define separators, orientation, protective material and dryness. Confirm that packaging does not transfer residue or mark the visible face.
Inspect after the expected shipping and line-side handling sequence, not only at the finisher. Packaging cost belongs in the finish system because a perfect plated part that arrives scuffed is not an accepted product.
Hardware production release
Named Zamak grade, function zones and visible classes.
Loaded mechanism, handle proof/abuse and fastener torque tests.
Wear pair, lubricant, contamination and cycle endpoints.
Substrate, polish, layer stack, appearance and corrosion evidence.
Finished hole spacing, spindle/lock fit and assembled operating force.
Packaging that prevents part-on-part finish damage.
Where the product contains multiple castings and purchased pieces, an assembly plan should control torque, orientation, lubrication and final function. Zinc is suitable because it can place mechanism and appearance in one compact product, provided each of those functions has its own acceptance evidence.