Why is zinc die casting widely used for automotive components?
Zinc die casting is widely used for selected automotive components because compact latch, lock, handle, trim and connector parts often need dense integrated features, repeatable assembly locations and a controlled decorative or protective finish at high production volume. Zinc is not a default for every vehicle part. Mass, sustained temperature, vibration, corrosion, load path and vehicle-level validation must suit the named Zamak alloy and finished design.
Where zinc fits in a vehicle
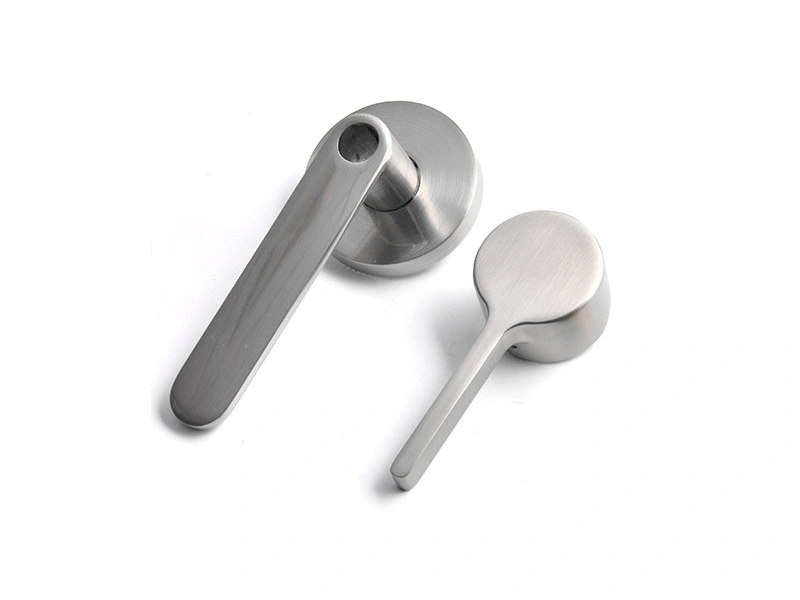
Typical candidates include door-handle structures, latch and lock pieces, interior control hardware, trim carriers, seat-adjustment mechanisms, sensor or connector shells and small mounting components. These parts can integrate pivots, stops, spring pockets, bosses, apertures, screw locations and visible contour. A well-designed casting may replace several pieces and reduce alignment stack-up.
Location matters. A cabin control, exterior handle and under-hood bracket experience different heat, water, chemicals and vibration. The zinc die casting route should be screened against the actual mounting zone, not a generic automotive classification.
Part-family decision table
Part family | Why zinc may fit | Dominant risk | Release evidence |
|---|---|---|---|
Exterior or interior handle structure | Ergonomic form, bosses and plated/painted visible zones | Installation torque, abuse load, wear and edge corrosion | Load/cycle, finish exposure and vehicle-door assembly |
Latch or lock component | Compact stops, pivots and spring interfaces | Impact, burr interference, wear and cold/hot movement | Duty cycle with mating parts across environment |
Connector or sensor shell | Terminal alignment, conductive enclosure and small apertures | Vibration fretting, lost ground and seal fit | Mating, vibration, electrical and ingress tests |
Decorative trim carrier | Crisp form and controlled finishing base | Substrate print-through, rack marks and coating damage | Limit sample, adhesion and environmental exposure |
Integrated features create the automotive value
Zinc filling behavior can support detailed geometry in a small envelope. The economic benefit appears when cast bosses, stops or locating features remove machining, welding, separate brackets or assembly fixtures. Count those avoided operations when comparing processes.
Integration also concentrates risk. A pore at a machined thread, a burr beside a latch path or distortion at a connector window can reject the complete component. Review gate-to-vent flow, trim, ejection and function-sensitive zones before tooling. The published automotive handle application is a design direction, not evidence for a different part.
Temperature and mass can reject zinc
Zinc's higher density can be a penalty when many parts multiply mass across a vehicle or when the component envelope grows. Calculate installed mass including inserts and finish. If low mass drives the system, aluminum, polymer, sheet metal or another route may deserve priority.
Define normal and transient temperature, load and dwell. A loaded zinc boss near a motor or heater requires time-temperature deformation evidence; room-temperature tensile data do not prove retention. High-heat structural or thermal-management components are commonly outside zinc's strongest application space.
Finish and corrosion are complete systems
Automotive zinc hardware may be plated, painted or powder coated, depending on appearance and location. Performance comes from alloy purity, substrate integrity, preparation, layer stack, edges, rack marks, fastener damage and exposure. A coating cannot repair a crack or cold shut.
Specify the full route, visible zones, color or metallic appearance, wear points and corrosion endpoints. Test final parts with representative installation damage where the customer method requires it. The zinc finishing guide explains why topcoat names alone are insufficient.
Assembly, vibration and function
Use production fasteners, torque tools, clips, springs, seals and mating parts. Measure clamp load or engagement where relevant. Vibration testing should use the installed orientation and harness or connector mass because interface motion can dominate. Inspect for fretting, cracks, loose fasteners, electrical change and finish damage afterward.
Latch and handle cycle tests need the specified load, misalignment, contamination and temperature. A no-load bench cycle can miss boss loading or door-system deflection. Define acceptable force, free play, wear and final appearance before testing.
Diagnose failures by vehicle interface
A cracked boss beside a mounting screw, a worn latch stop and blistered plating near a drain path require different corrections. Record defect position, cavity, casting lot, finishing lot, assembly torque and vehicle location. Section or measure the affected zone where visual evidence cannot separate a substrate discontinuity from overload, coating preparation or interface motion.
Correct the responsible level. A repeated pore at one boss points to tool or casting control; finish damage under a moving clip points to interface design; connector fretting may require harness support or contact changes. Adding inspection without diagnosing the interface can preserve the failure.
Automotive RFQ inputs
Provide vehicle location, installed orientation, mass target, load and misuse cases, vibration input, temperature profile, chemicals, corrosion class, mating metals and desired appearance. Mark security-, safety- or fit-sensitive characteristics and identify required customer approval records. State packaging and line-side handling because plated faces and latch edges can be damaged before installation.
Production and change evidence
Named zinc grade, chemistry verification and lot traceability.
Cavity identity, tool state, casting and trim process controls.
Function-sensitive dimensions after machining and finish.
Substrate and finished appearance by visible class.
Component and vehicle-level validation specified by the customer.
Notification triggers for alloy source, tool, machining, finish and assembly changes.
If a customer production-part approval process applies, its exact records and submission level belong in the RFQ. Do not claim that every zinc casting is automatically compliant. Zinc is widely used because it can satisfy compact automotive hardware needs efficiently when these controls are built into the project.