OEM Die Casting Parts: Drawing Control, Tooling Ownership and Production Records
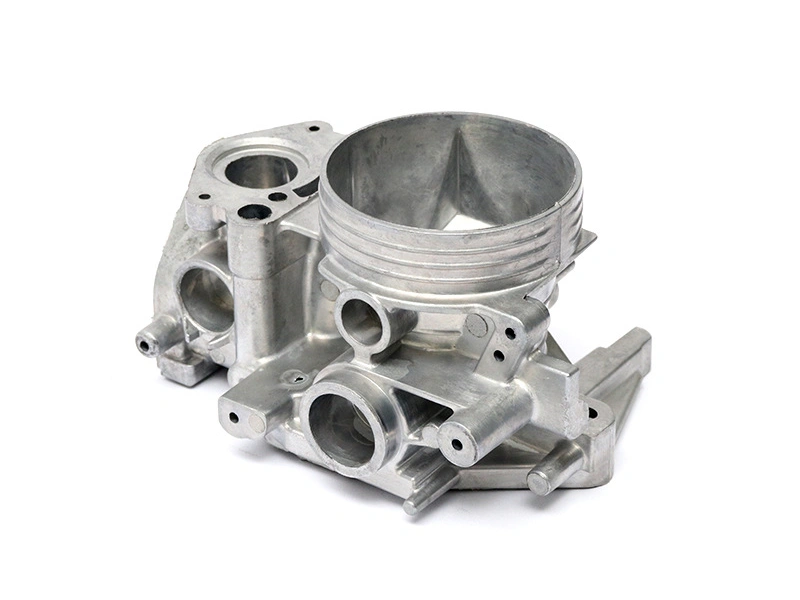
OEM die casting parts should be released as a controlled product and process package, not as a shape file sent with a quantity. The package needs the approved drawing, 3D model, alloy and condition, functional datums, casting and machining state, finish, inspection method, packaging, and change-approval rules. The die-casting route can then be selected against the actual part and production requirement. A supplier may be able to cast the geometry, but the OEM decision also depends on who controls the tool, how a revision is identified, which records follow the lot, and how a process change is approved.
The most useful early review connects each drawing requirement to an operation and to evidence. A sealing land may be cast and then machined; a cosmetic wall may remain as-cast; a threaded hole may need machining and a gauge; and a pressure boundary may need a leak test on the finished part. OEM die casting becomes predictable when those states are written down. If the buyer leaves them implicit, quotations that appear comparable can include different levels of tooling, machining, inspection, and warranty risk.
Release the Drawing Before Releasing the Tool
Start with the revision that governs the purchase. The drawing should identify the material designation, casting process if it is fixed, heat-treatment or condition requirements, surface treatment, part marking, and the measurement state. The 3D model should carry the same revision identity as the 2D drawing. If the model is nominal and the drawing controls dimensions, say so. If the model controls a profile or freeform surface, state that relationship. This prevents a toolmaker from cutting steel from a file that the buyer later considers only reference geometry.
Next, map the features to their production state. A hole shown in the model may be cored, cast with a pilot, drilled, reamed, or machined with a thread. The choice affects tool cost, cycle, stock, inspection, and the risk of opening a subsurface defect. A large flat face may be acceptable as-cast for a cover but require milling for a gasket. The RFQ should identify which dimensions are evaluated on the raw casting and which are evaluated after trimming, machining, coating, or assembly.
Define Datums From the Assembly
OEM parts often fail at interfaces rather than at their overall envelope. A mounting pad, locating boss, bearing bore, connector opening, or sealing face establishes how the part fits into the next assembly. The drawing should make those relationships clear and the supplier should show how the raw casting will be located for machining. A flexible wall should not be pushed into position by a fixture and then reported as though it were naturally stable. The measurement result has meaning only when the support and datum basis are stated.
Datum control also affects tool design. If a parting line crosses an interface, flash or mismatch may enter the machining stock or remain on the finished face. If a core forms a long passage, core shift may change the wall relative to the outside mounting features. If ejectors push on a thin cosmetic wall, the part may move after release. The DFM review should mark these relationships on the model and agree which effects are removed by machining and which remain part of as-cast acceptance.
| OEM requirement | Production decision | Evidence to request |
|---|---|---|
| Mounting or locating interface | Choose casting datum, machining setup, and fixture support | Datum plan, fixture description, dimensional report |
| Pressure or sealing feature | Control wall, stock removal, surface, and test state | Finished-part leak or pressure result and defect disposition |
| Cosmetic face | Set parting, gate, trimming, cleaning, and finish boundaries | Approved visual sample and finish inspection record |
| High-volume repeat part | Define tool maintenance, lot traceability, and change approval | Tool history, process record, and revision-controlled release |
Tooling Ownership Needs More Than a Name on an Invoice
Tool ownership should cover physical custody, design files, revisions, maintenance, spare inserts, storage, and release of repairs. The buyer should know whether the tool is dedicated to one part, whether the supplier may use it for another customer, and who authorizes a geometry change. A tool can be paid for by the OEM and still be difficult to transfer if the cavity model, electrode data, inspection records, and maintenance history are not included in the agreed deliverable.
Ask for a tool identification scheme that ties cavity, insert, slide, and core numbers to the assembly drawing. This helps when one insert is repaired or replaced while the rest of the tool remains unchanged. The repair record should describe the area, reason, action, and post-repair check. Without that record, a later flash or dimensional shift may be blamed on the casting process when the real change was a shutoff repair or insert rework.
Maintenance Is Part of the Production Price
Die casting tools need cleaning, inspection, lubrication where applicable, and repair based on the alloy, cycle, thermal history, and wear areas. The production quote should state which routine work is included and what triggers a chargeable correction. Gate edges, vents, slides, ejectors, cooling passages, and shutoffs do not have the same maintenance need. A blanket statement that the tool is maintained “as required” gives the buyer no way to compare capacity or plan downtime.
Neway's tool and die making route can be evaluated with the OEM tool scope. The buyer should retain the approved tool design, trial revision, maintenance assumptions, and ownership terms. That record is useful even when the supplier continues to run the tool because it defines what the buyer is actually purchasing.
Validation Records Should Follow the Part Through Its States
An OEM validation package should distinguish design feasibility, tool trial, process approval, and ongoing production checks. A first casting can show that the cavity fills, yet the machined component can still fail because stock is insufficient or the fixture shifts a datum. A finished sample can meet dimensions while the tool contains a vent or cooling issue that will become visible after maintenance. Record the sample condition, tool revision, alloy lot, process state, machining setup, finish, and inspection method for each stage.
Inspection should be chosen for the failure mode. Visual checks can identify flash, cold shuts, surface laps, and handling marks. Dimensional checks can confirm interfaces and overall shape. Leak testing can address a defined pressure boundary. Internal examination may be selected for a known subsurface risk. No single certificate proves every requirement. The buyer should ask why each method is included and what result would cause a process review or part rejection.
Make Traceability Useful at the Assembly Level
Lot identification is useful when it can be connected to material, tool, process, machining, finish, and inspection records. The mark may be a code, cavity reference, date or lot identifier, or another method approved by the customer. It should not damage a sealing face or change the balance of a rotating part. The record should explain what the identifier means and how a nonconforming lot is contained.
For an assembled OEM product, also define how cast parts are separated from hardware, seals, inserts, and coatings in the traceability system. A leak failure may originate in the casting, machining, seal, or assembly torque. If all are bundled under one part number with no process history, corrective action becomes guesswork. A staged record makes the investigation faster and protects the buyer from repeating a fix that addressed the wrong operation.
Change Control Protects the Approved Part
Changes that appear small can alter an OEM die casting part. A gate may move, an overflow may be removed, a core may be changed, a machining tool may be replaced, or a coating pretreatment may be adjusted. Each change can affect dimensions, porosity, surface, cycle, or assembly. The purchase terms should define which changes require prior approval, which can be handled as routine maintenance, and what evidence is required before the changed process returns to production.
Revision control should cover the drawing, 3D model, tool design, process sheet, inspection plan, control plan where used, and packaging instruction. Use one revision identity across the documents. When a supplier suggests an alternative alloy, process, or finish, the request should state the affected requirement and the evidence supporting the change. This keeps a commercial cost reduction from becoming an undocumented technical substitution.
RFQ Inputs for OEM Die Casting Parts
Provide the approved drawing and model, alloy and condition, annual and launch quantities, functional interfaces, cosmetic surfaces, expected casting state, machining requirements, finish, inspection, packaging, marking, and change rules. State whether the supplier is expected to provide tooling, machining, assembly, or only cast blanks. Include any customer-specific material or restricted-substance requirements and identify which results are needed for sample approval.
Ask the supplier to return a marked-up DFM review, tool concept, process route, machining datum plan, inspection proposal, maintenance scope, and schedule assumptions. A quote from Neway's aluminum die-casting route can be compared more fairly when each operation and evidence package is visible. The buyer can then decide whether a lower unit price includes the same level of production control.
Use the DFM Review to Freeze the Right Decisions
The DFM review is the point where the OEM, tool designer, casting engineer, machining engineer, and quality representative should look at the same revision. Mark the proposed parting line, gates, overflows, vents, slides, cores, ejectors, draft, ribs, bosses, and machining stock. Then mark the features that cannot move because of an assembly, sealing, electrical, thermal, or cosmetic requirement. A feature that is easy to cast but difficult to inspect may not be the best feature for the production release.
Do not approve a DFM report that only lists possible changes. Each proposed change should state the requirement it protects and the effect on cost, tooling, machining, or appearance. A rib may be thickened to support a load path, but it can create a heavy section and a local shrinkage risk. A hole may be moved away from a parting line, but the relocation may affect the mating bracket. The buyer can approve a change quickly when the engineering reason and commercial effect are shown together.
Keep Simulation, Trial, and Physical Inspection Connected
Flow or solidification simulation can help identify a difficult fill path, a potential hot spot, or a gate and overflow concept. It is a design aid, not physical proof of the finished part. The model input should identify alloy, geometry revision, assumed process, and boundary conditions. When the actual tool or process changes, the result may need to be revisited. A physical trial then checks the features the analysis identified, followed by dimensional, surface, internal, leak, or functional inspection as required.
FEA or casting simulation should not be used to create a promise that the buyer did not specify. Ask what decision the analysis supports: a wall change, a gate location, a core arrangement, a machining datum, or a test selection. The final validation package should keep the analytical file, tool revision, physical sample, and inspection report traceable. Neway's engineering solutions route can be reviewed when the OEM needs design and casting decisions assessed together.
Make the Cost Model Match the Deliverable
OEM quotes should distinguish nonrecurring tooling and engineering from recurring part cost. Tooling may include design, steel, inserts, electrodes, heat treatment, assembly, trial, correction, and storage. Recurring cost may include alloy, casting, trimming, machining, finishing, inspection, packaging, and maintenance. If a supplier combines all of these into one unit price, the buyer cannot see which change will affect the program or compare a tool transfer later.
Machining scope is especially important. A cast blank may be inexpensive while a finished housing requires several setups, special fixtures, deburring, washing, and inspection. A finish can add masking and handling that are not visible in the raw casting quote. Ask the supplier to identify assumptions about scrap, rework, sample parts, and packaging. Neway's post-process finishing route can be included when the delivered part needs a controlled surface rather than only a cast appearance.
Plan the Handoff From Validation to Production
Production release should list the approved drawing and model revision, material, tool identity, process route, machining program, finish, inspection plan, packaging, and records. It should also identify open items, temporary deviations, and the date or condition under which they close. A sample approval that has no link to the production revision is difficult to enforce. The buyer should require a clear statement that the production process matches the approved sample or identify the approved differences.
Packaging deserves a technical review for machined and finished castings. Parts can be scratched, dented, contaminated, or mixed by cavity and lot during transport. The package should protect functional surfaces, preserve part marks, and keep finished parts separate from unfinished or rejected material. If cleanliness is required before assembly, state the cleaning state and how it is verified. Neway's post-machining route can be reviewed with the packaging and inspection state so that the delivered part is not confused with the rough casting.
Control Deviations Without Losing the Product Definition
Deviations are sometimes needed during launch, but each one should identify the affected drawing note, part feature, quantity, duration, and disposition. A temporary allowance on a cosmetic face is different from a change to a pressure boundary or locating hole. The buyer should know whether the deviation is limited to a sample, a lot, or a date range and what evidence is required before normal production resumes.
Nonconforming parts should be separated by the same identifiers used for traceability. If a defect is found after machining, preserve the raw and finished samples where practical. This helps the team identify whether the cause came from metal, tool, trimming, fixture, machining, finish, or assembly. Corrective action is more useful when it changes a controlled process step and verifies the affected feature instead of simply sorting the next lot.
OEM die casting parts are easier to manage when the technical and commercial boundaries are visible. Include the approved product definition, tool records, process evidence, finished state, and change rules in the purchase package. That gives the supplier a precise route and gives the OEM a defensible record when the program moves from launch to ongoing production.
Keep Launch Records Separate From Marketing Claims
At launch, retain the approved sample, drawing and model revision, tool identity, material record, machining state, finish, inspection, and deviation list. These records describe what was actually approved. They are more useful to an OEM than an unsupported claim about capacity or delivery because they can be checked when the product or process changes.
Approve the Sample in the State the OEM Will Receive
If the customer receives a machined, finished, or assembled part, approve that state. A raw casting sample can support process learning but cannot replace inspection of the delivered interface.
Buyer Summary
OEM die casting parts are controlled products. Their quality depends on drawing release, casting and machining states, tooling ownership, datums, validation, traceability, and change approval. A supplier should explain how the drawing becomes a repeatable process and how the evidence follows the part into production.
Define the interfaces, tool records, material evidence, inspection state, and repair path before steel cutting. That gives design, purchasing, and quality teams one shared basis for approving an OEM die-casting program.
FAQ